
Services · Machining
Precision CNC Machining and Conventional Machining
TSIRIKOS machines industrial components to your drawing or sample in its Piraeus workshop: CNC milling on horizontal and vertical machining centres, together with conventional turning, milling, horizontal boring, thread and spline cutting and grinding. Machining, gear cutting, heat treatment and inspection are carried out in the same plant.
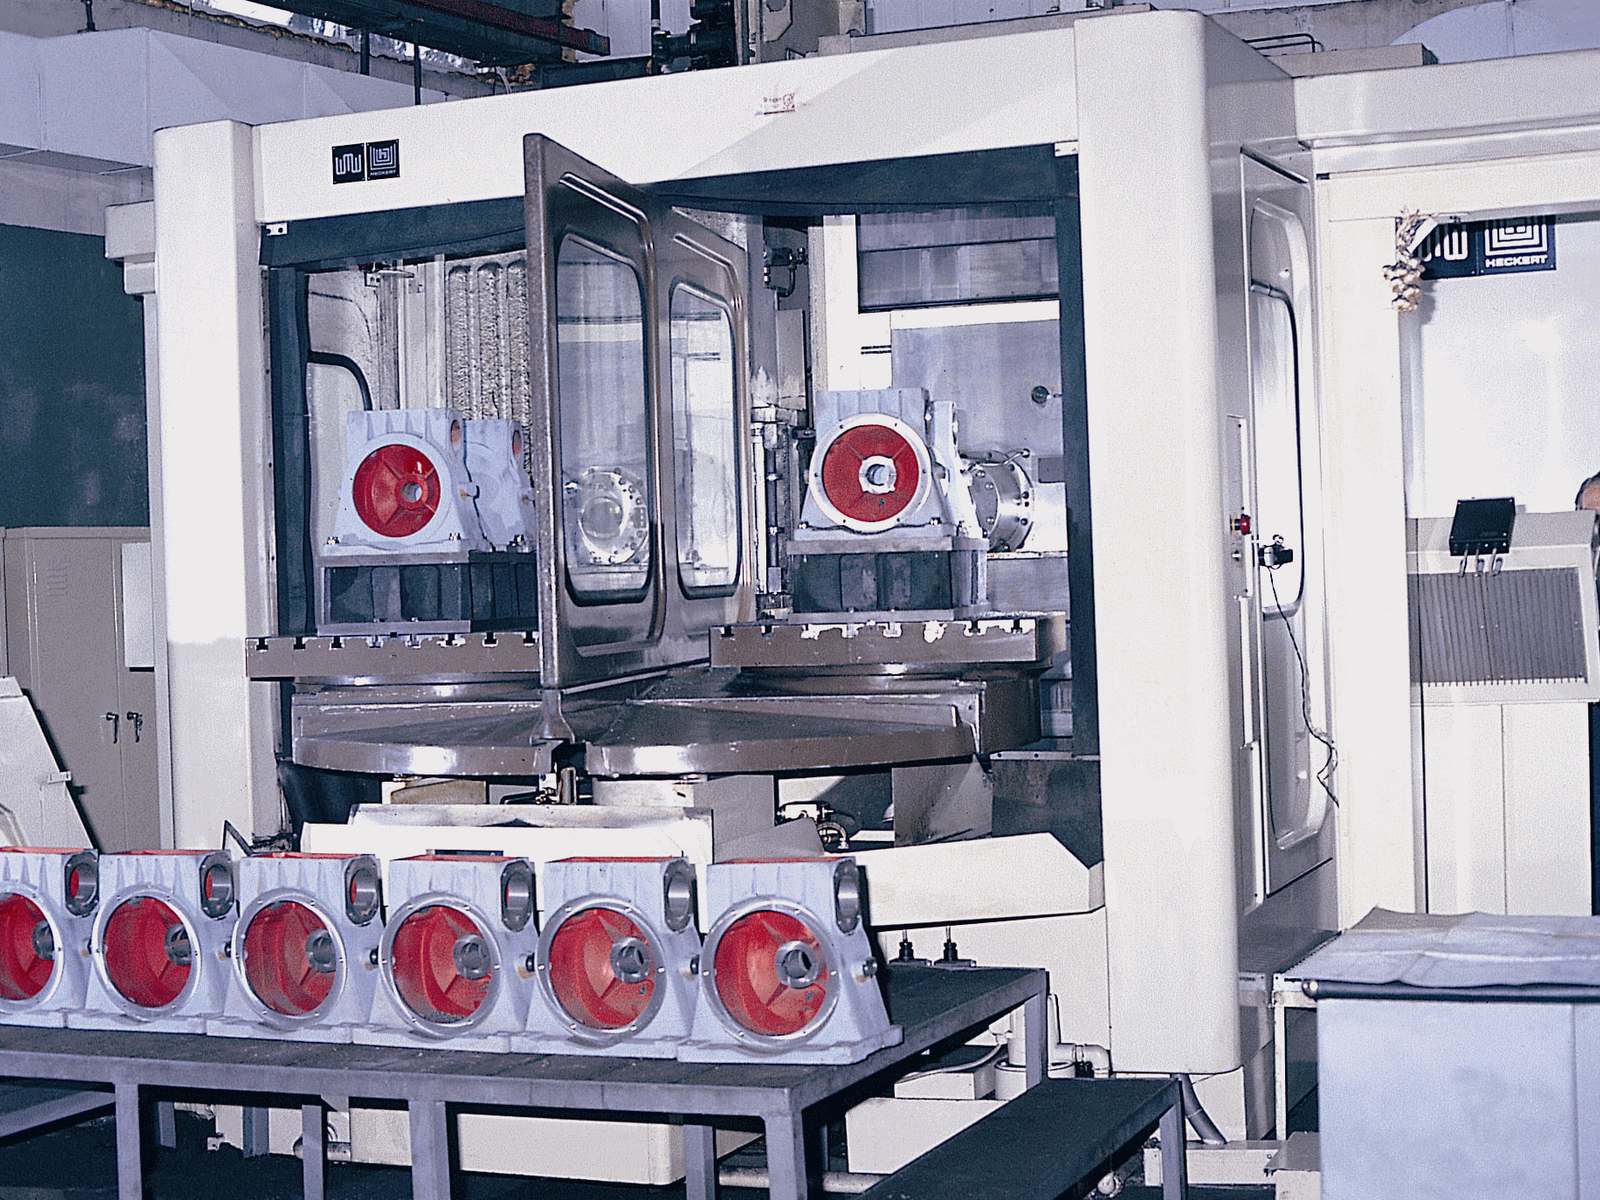
Main applications
-
Gearbox housings and pump bodies
Learn more : Gearbox housings and pump bodiesBearing bores, joint faces, threaded holes and oil passages machined on a horizontal machining centre, so that related features are produced in the same set-up.
-
Shafts, pinion shafts and spline shafts
Learn more : Shafts, pinion shafts and spline shaftsTurning, keyway milling, spline cutting and journal grinding of transmission shafts for gearboxes, mills, conveyors and pumps.
-
Rings, flanges, bushes and hubs
Learn more : Rings, flanges, bushes and hubsLarge-diameter turning and facing of rings, flanges, bushes and hubs, including bore and face grinding where the drawing requires it.
-
Large housings, drums and fabrications
Learn more : Large housings, drums and fabricationsHorizontal boring and milling of hubs, drums, welded frames and marine parts such as propeller blade flanges.
-
Extruder screws and barrels
Learn more : Extruder screws and barrelsTurning, flight machining and grinding of extruder screws and barrels for plastics machinery, an activity of the company since 1985.
Machining operations
-
CNC milling, drilling and tapping
Prismatic parts machined on CNC horizontal and vertical machining centres, with conventional universal milling machines for one-off and repair work.
-
Machine park
Two 4-axis CNC machining centres, a 3-axis CNC vertical milling machine and a number of conventional universal milling machines.
-
Horizontal machining centre, 4 axes, 60 tools
A WMW horizontal machining centre with 4 axes, a 60-tool automatic changer and a double pallet table machines gearbox housings and pump bodies.
-
Maximum workpiece size 3.5 × 7 × 5 m
Workpiece volume for milling. The machine and set-up are chosen according to the dimensions and weight of each part.
-
Turning
Turning of shafts, rings, discs and large-diameter parts on conventional and heavy facing lathes.
-
Horizontal boring
Boring and facing of housings, hubs and large fabrications where bore alignment and distance between bores matter.
-
Thread and spline cutting
External and internal threads, and internal and external splines on shafts, gears and hubs.
-
Grinding
Internal and external cylindrical grinding, surface grinding, grinding of long shafts and rolls, large-diameter rings, worms and extruder screws and barrels.
-
Gear cutting and gear grinding
Learn more : Gear cutting and gear grindingGear teeth are cut and, where specified, ground in-house; see industrial gears for the gear types.
What we machine
Our machining work is focused on components for power transmission and industrial machinery: gearbox housings and covers, pump bodies, shafts and pinion shafts, rings, flanges, bushes, hubs, drums and gear blanks. Everything is made to the customer’s drawing or to a sample. We do not sell catalogue parts, so each job starts with your drawing, your material and your tolerances.
Typical requests come from maintenance departments that need a replacement part for an existing machine, from engineering offices that need a prototype or a small batch, and from equipment builders that need a complete machined and heat-treated component rather than a raw part.
CNC and conventional machining, used where each fits
CNC machining centres are the right tool for prismatic parts with many related features. On a horizontal machining centre, bearing bores, faces, threaded holes and oil passages of a gearbox housing can be produced in one set-up, which keeps bore alignment and centre distance under control.
Conventional machines remain essential in an industrial machine shop. Single replacement parts, very large or heavy parts, and repair work on worn components are often faster and safer on a conventional lathe, milling machine or horizontal boring mill operated by an experienced machinist.
Typical operations in our workshop:
- turning of shafts, rings, discs and large-diameter parts;
- CNC milling, drilling and tapping on horizontal and vertical machining centres;
- horizontal boring of housings, hubs and fabrications;
- thread cutting and internal or external spline cutting;
- cylindrical (internal and external), surface, worm and screw grinding.
Machining and heat treatment in one sequence
For hardened parts, the order of operations decides the result. A carburized gear or shaft distorts during quenching, so it is rough-machined with an allowance, heat-treated, and then finished by grinding. A nitrided part distorts much less, but it must be machined to near-final size before treatment because the hard layer is thin.
Because heat treatment, gear cutting and grinding are carried out in the same plant, we plan the allowances, the heat-treatment cycle and the finishing operations together, without sending the part to several subcontractors.
Tolerances, roughness and inspection
Tolerances and surface finish come from your drawing. Tell us which dimensions are functional (bearing seats, sealing diameters, bores, centre distances) and which are free; this is often the difference between a sensible price and an over-engineered one. Parts are checked for dimensions, surface roughness and, after heat treatment, hardness before dispatch.
What to send with your request
- A dimensioned drawing (PDF) and, if available, a CAD file (STEP, DWG or DXF).
- Material, heat treatment and surface treatment.
- Quantity and required inspection documents.
- The machine or application the part belongs to.
If you have no drawing, our manufacturing from drawings and reverse engineering services explain how we work from a sample. See also custom machined components and shafts and pinion shafts, or go straight to the request for quotation.
Materials
-
Carbon and alloy steels
Low, medium and high carbon steels, case-hardening, through-hardening and nitriding steels.
-
Stainless steels and nickel alloys
For corrosive or high-temperature service, as specified on the drawing.
-
Non-ferrous metals and plastics
Aluminium, copper, brass and PTFE (Teflon) components.
Materials we machine regularly. Special steels are selected and imported according to the application and the part requirements.
How we work
-
Drawing review
We check dimensions, tolerances, material, heat treatment and surface finish, and ask questions before quoting if anything is unclear.
-
Material and blank
Bar, forging, casting or plate is selected according to the drawing; material certificates are requested from the supplier where required.
-
Rough machining
Parts that will be hardened are rough-machined with allowance for heat-treatment distortion and finishing.
-
Heat treatment
Carburizing, nitriding, induction hardening or quenching and tempering in our own heat-treatment department, when specified.
-
Finish machining and grinding
Bearing seats, bores, faces and teeth are finished to the drawing tolerances and roughness values.
-
Inspection and dispatch
Dimensional, roughness and hardness checks before the part is packed and dispatched.
Quality considerations
-
Dimensional inspection
Dimensions checked with calibrated micrometers; concentricity, parallelism, eccentricity and ovality with precision measuring instruments.
-
Surface roughness
Roughness measured after final machining and grinding with a calibrated digital roughness tester.
-
Hardness and crack examination
Surface hardness measured after heat treatment and surfaces examined for micro-cracks.
-
Inspection documents
Inspection documents according to EN 10204 (types 2.1, 2.2, 3.1, and 3.2 with the participation of an independent inspector), agreed per order.
Representative images
-
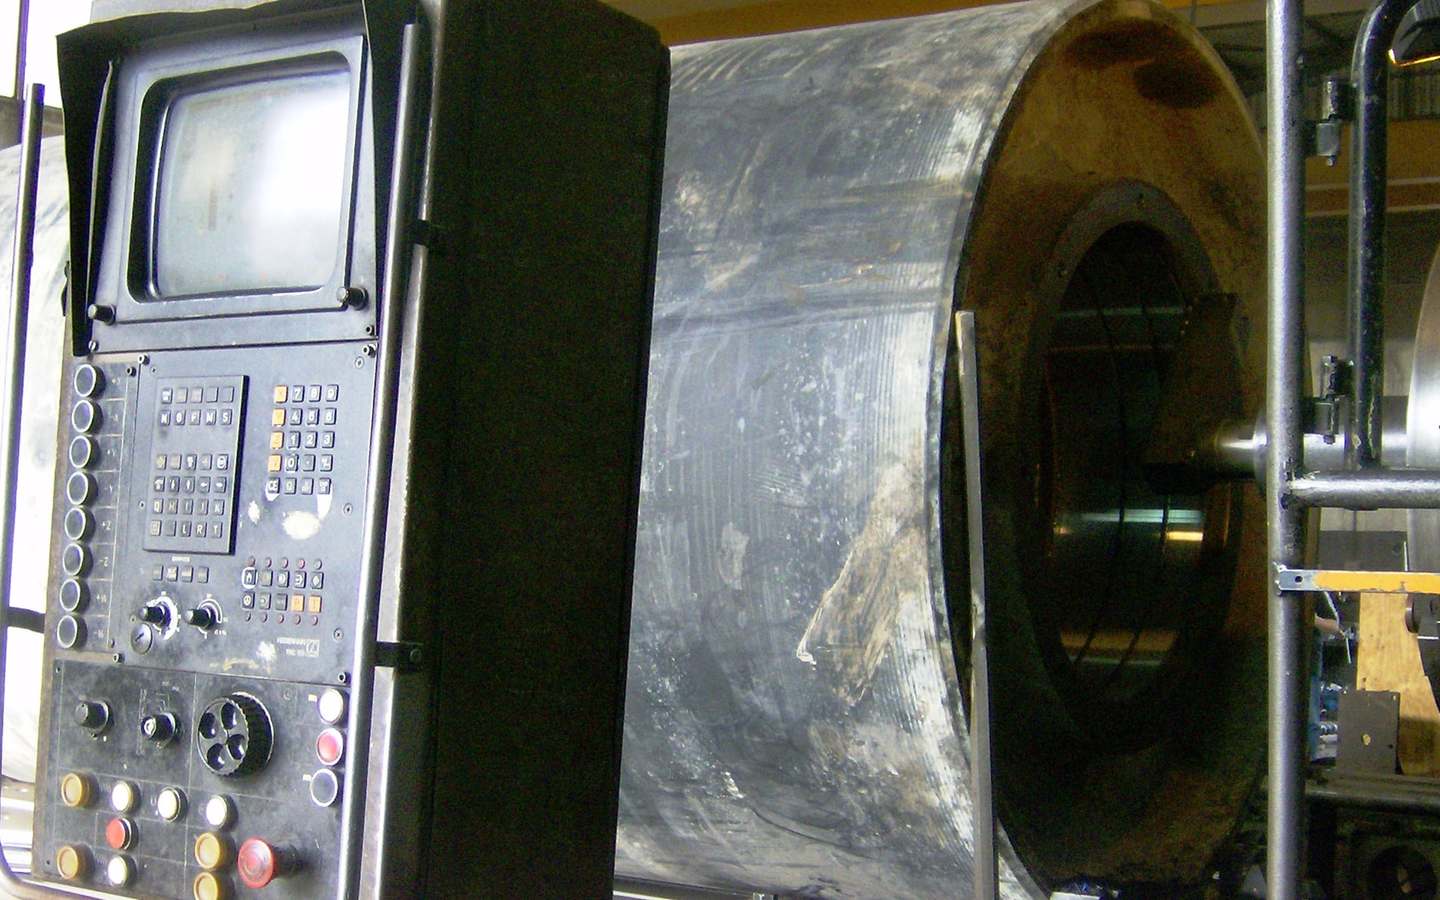
Large drum on a horizontal boring machine with Heidenhain CNC control -
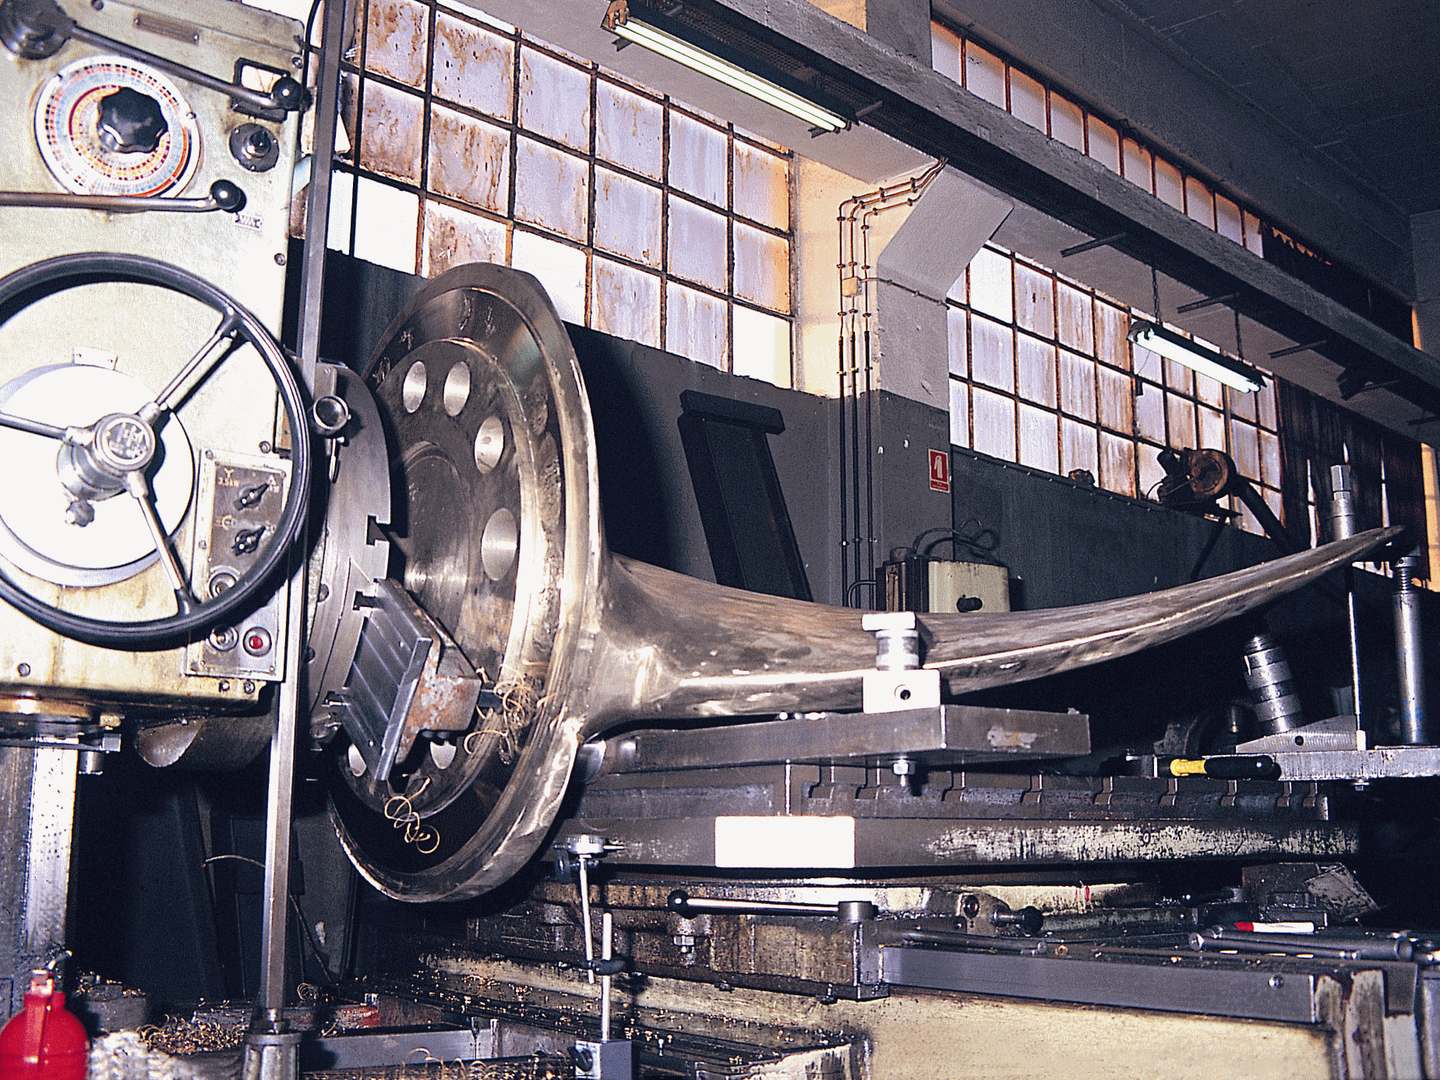
Marine propeller blade flange machined on a horizontal boring mill -
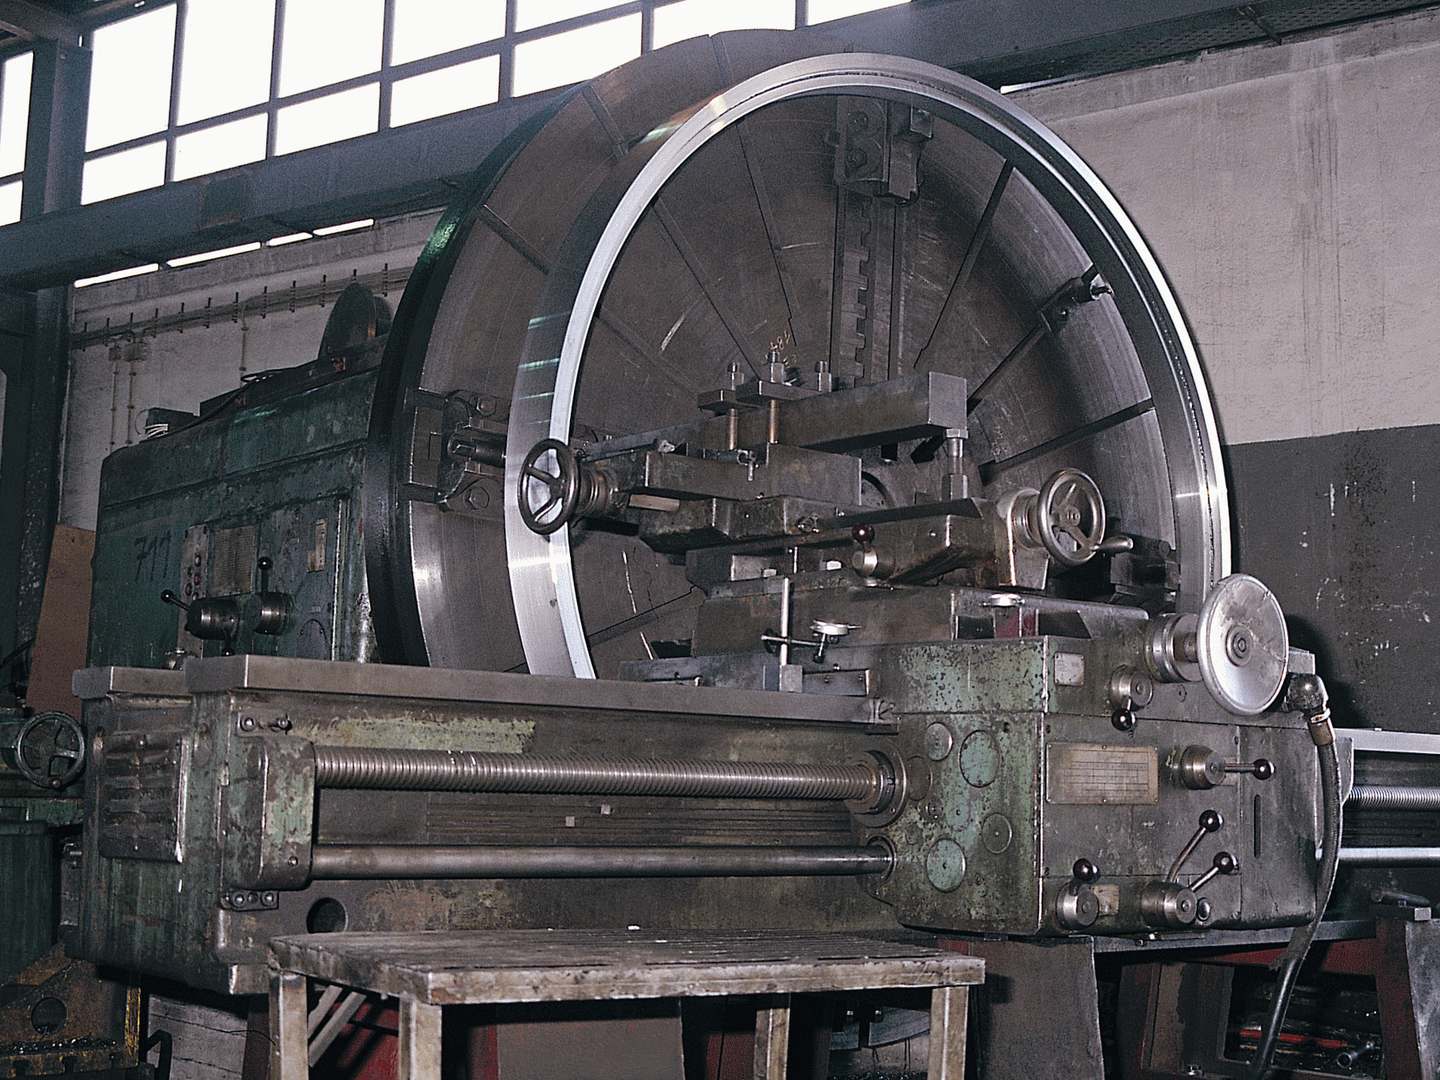
Large steel ring clamped on the faceplate of a heavy facing lathe -
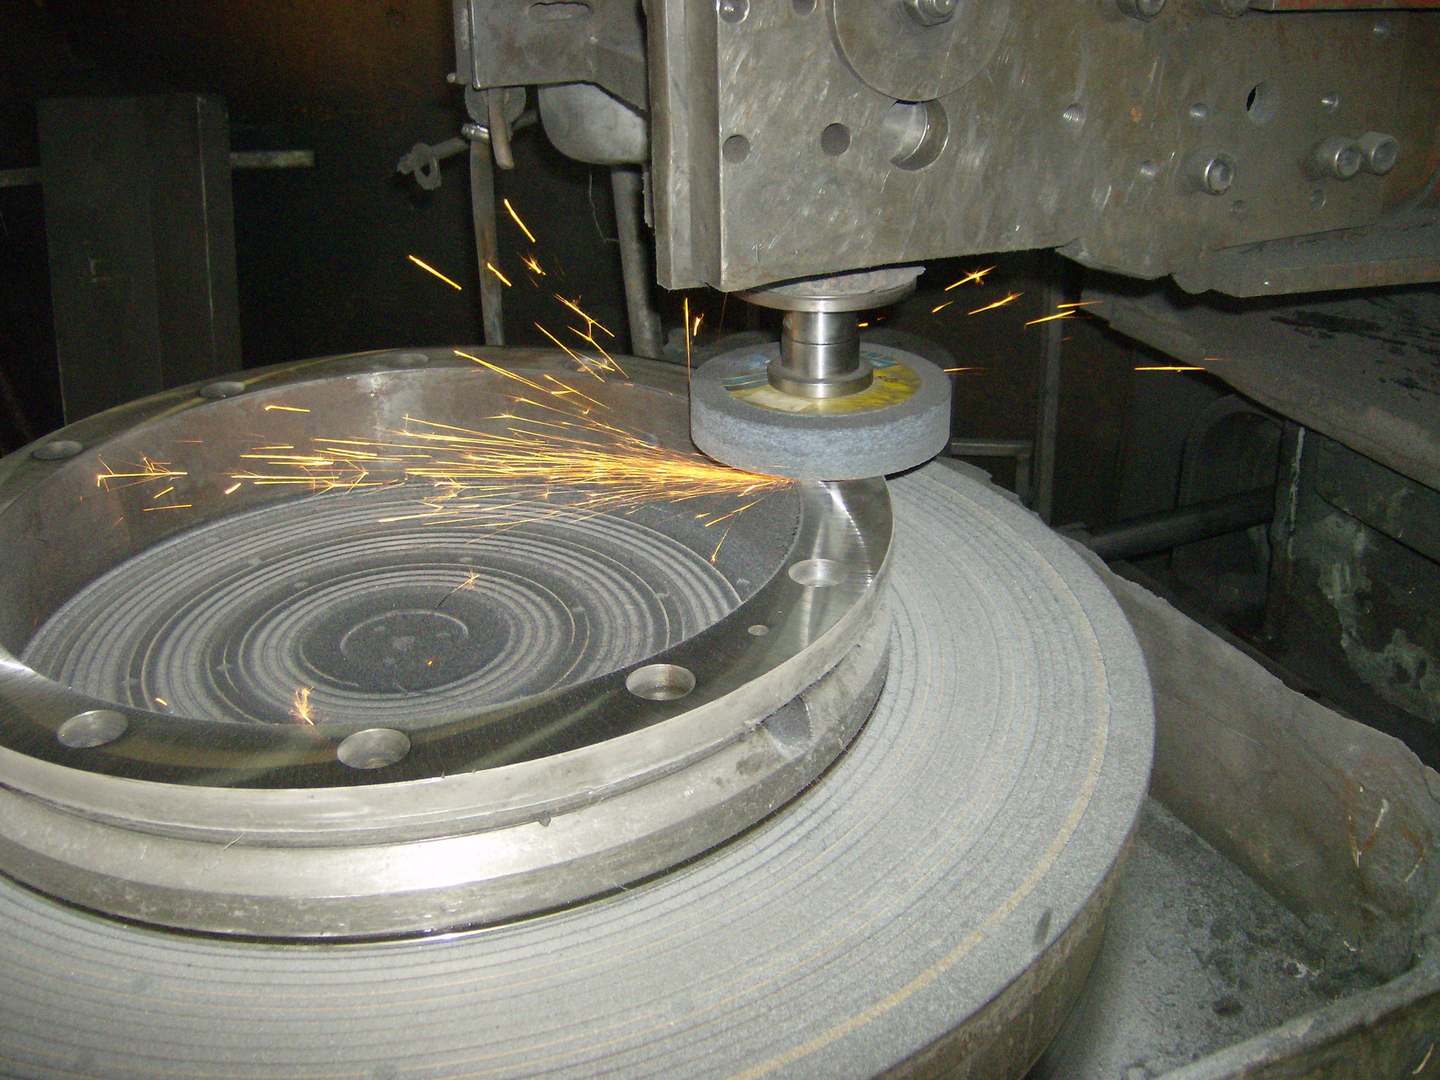
Grinding the face of a large flange ring, with sparks flying
Technical FAQ
Do you machine one-off parts or only series?
Most of our work is single parts and small batches made to the customer’s drawing or sample, typically spare parts and components for industrial machinery. Larger batches are quoted case by case.
Can you machine a part and also heat-treat and grind it?
Yes. Heat treatment and grinding are in-house, so a part can be rough-machined, carburized, nitrided or induction-hardened and then ground in the same plant.
What is the largest part you can machine?
We mill parts within a workpiece volume of 3.5 × 7 × 5 m. Send us the dimensions and weight of your part and we will tell you which machine it goes on.
Which file formats do you accept?
A dimensioned PDF drawing is the reference document. CAD files in STEP, DWG or DXF are welcome in addition, as are photos of an existing part.
Do you supply material certificates and inspection reports?
Yes. We supply inspection documents according to EN 10204. Tell us in your request which document type you need, so that it is included in the quotation.
Related pages
Request for quotation — Precision CNC Machining and Conventional Machining
CNC milling on machining centres plus conventional turning, boring, thread cutting and grinding of shafts, housings, rings and gear blanks, made to drawing in Greece.
Please attach your technical drawings and specifications to your email.