
Capabilities
Manufacturing capabilities: gear design, machining, gear cutting, heat treatment, assembly and repair
TSIRIKOS can take an industrial gear, gearbox or mechanical component from drawing or sample to a finished, inspected part on one site: design and recalculation, machining, gear cutting and grinding, heat treatment, assembly, inspection and repair. This page summarises what we do in each process family and links to the detailed product and service pages.
Capabilities at a glance
Eight process families cover most requests we receive. Each card links to the page with the details.
-
Design and engineering
Learn more : Design and engineeringGear and gearbox design and recalculation for your application; review of customer drawings.
-
Machining
Learn more : MachiningTurning, CNC and conventional milling, horizontal boring, thread and spline cutting, grinding.
-
Gear cutting and grinding
Learn more : Gear cutting and grindingHobbing of spur, helical and double-helical gears, spiral bevel generation, worm wheels, tooth-flank grinding.
-
Heat treatment
Learn more : Heat treatmentGas carburizing, nitriding, nitrocarburizing, induction hardening, quenching and tempering in-house.
-
Inspection and testing
Learn more : Inspection and testingDimensional, hardness, roughness, crack and gear tooth form inspection; load tests of repaired gearboxes where required.
-
Repair and overhaul
Learn more : Repair and overhaulGearboxes, gears, shafts, pump components, extruder screws and barrels.
-
From drawing or sample
Learn more : From drawing or sampleManufacture to your drawing, or from a worn sample after measurement and drawing approval.
Design and engineering
Gear and gearbox design for your duty
Our gear and gearbox design department calculates new gear stages, recalculates existing ones when a part has to be replaced or upgraded, and reviews customer drawings before manufacture. We work to the ISO, DIN or AGMA method specified by the customer and take the real duty into account: power and torque peaks, speed, shock loads, lubrication, mounting, temperature and environment.
- Load capacity checks of spur, helical and bevel gears
- Selection of steel grade, heat treatment and case depth
- Production drawings from your data or from a measured sample
- Technical suggestions on customer designs before quotation
Machining
Turning, milling, boring and grinding
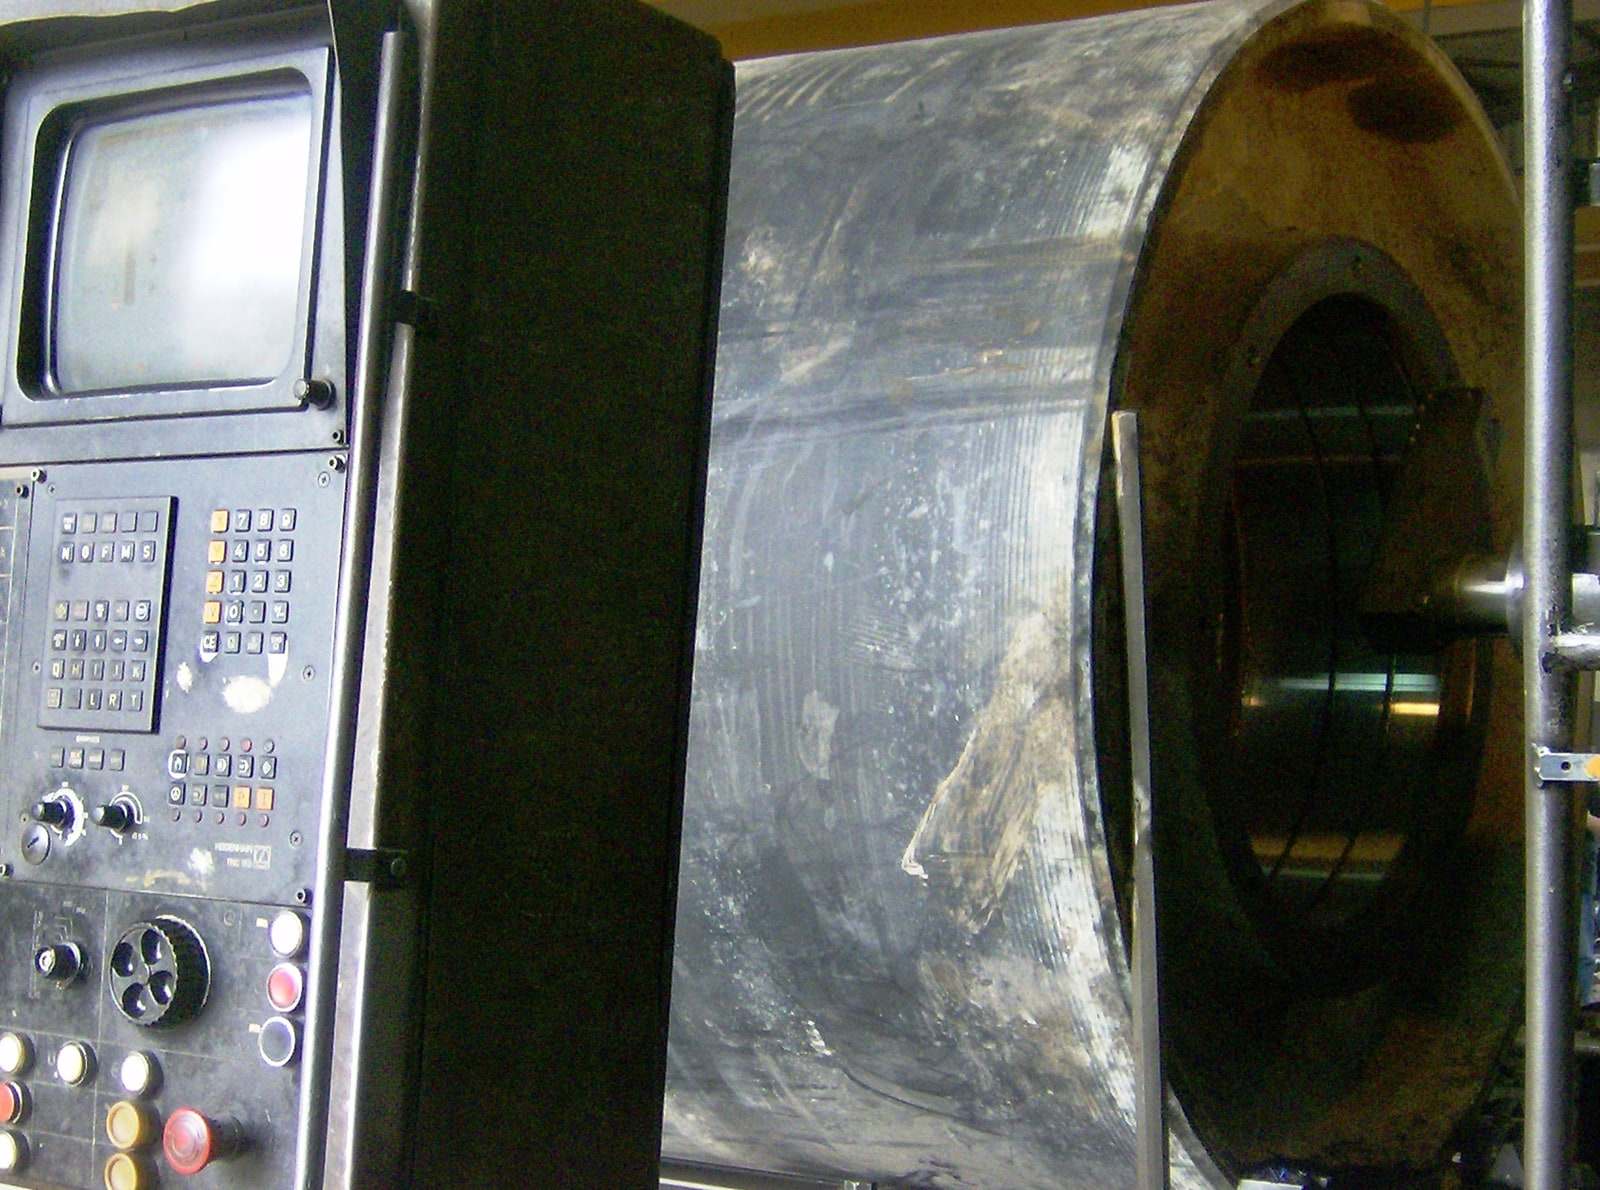
The machine shop covers conventional and CNC turning, milling on CNC machining centres and universal milling machines, horizontal boring of housings and large fabrications, thread and spline cutting, and grinding. Large rings, drums, propeller parts and gearbox housings are machined alongside small batches of shafts and bushes. Details are on the precision machining page.
- Turning of shafts, rings and large-diameter parts, including on a heavy facing lathe
- CNC machining centres for housings and pump bodies
- Horizontal boring of housings, hubs and drums
- External and internal spline cutting, thread cutting
- Cylindrical (internal and external), surface, worm and extruder screw grinding
Gear cutting and gear grinding
From hobbing to ground tooth flanks
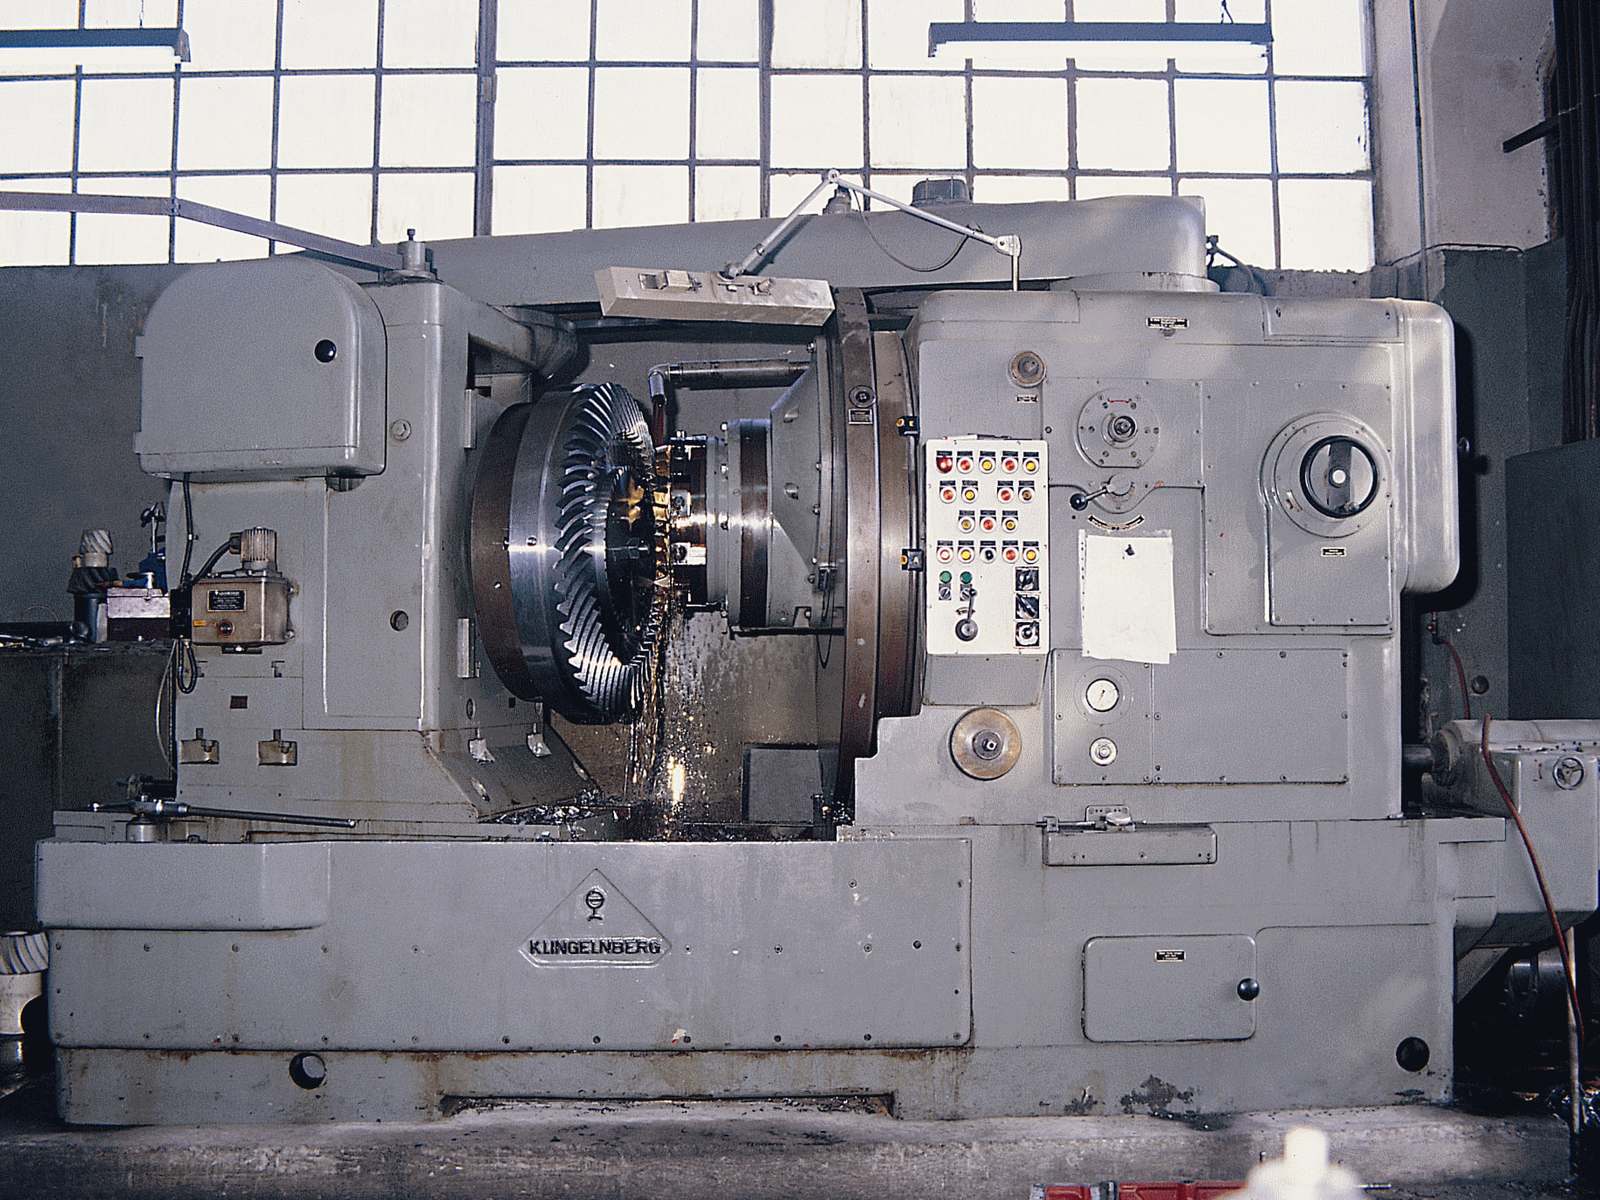
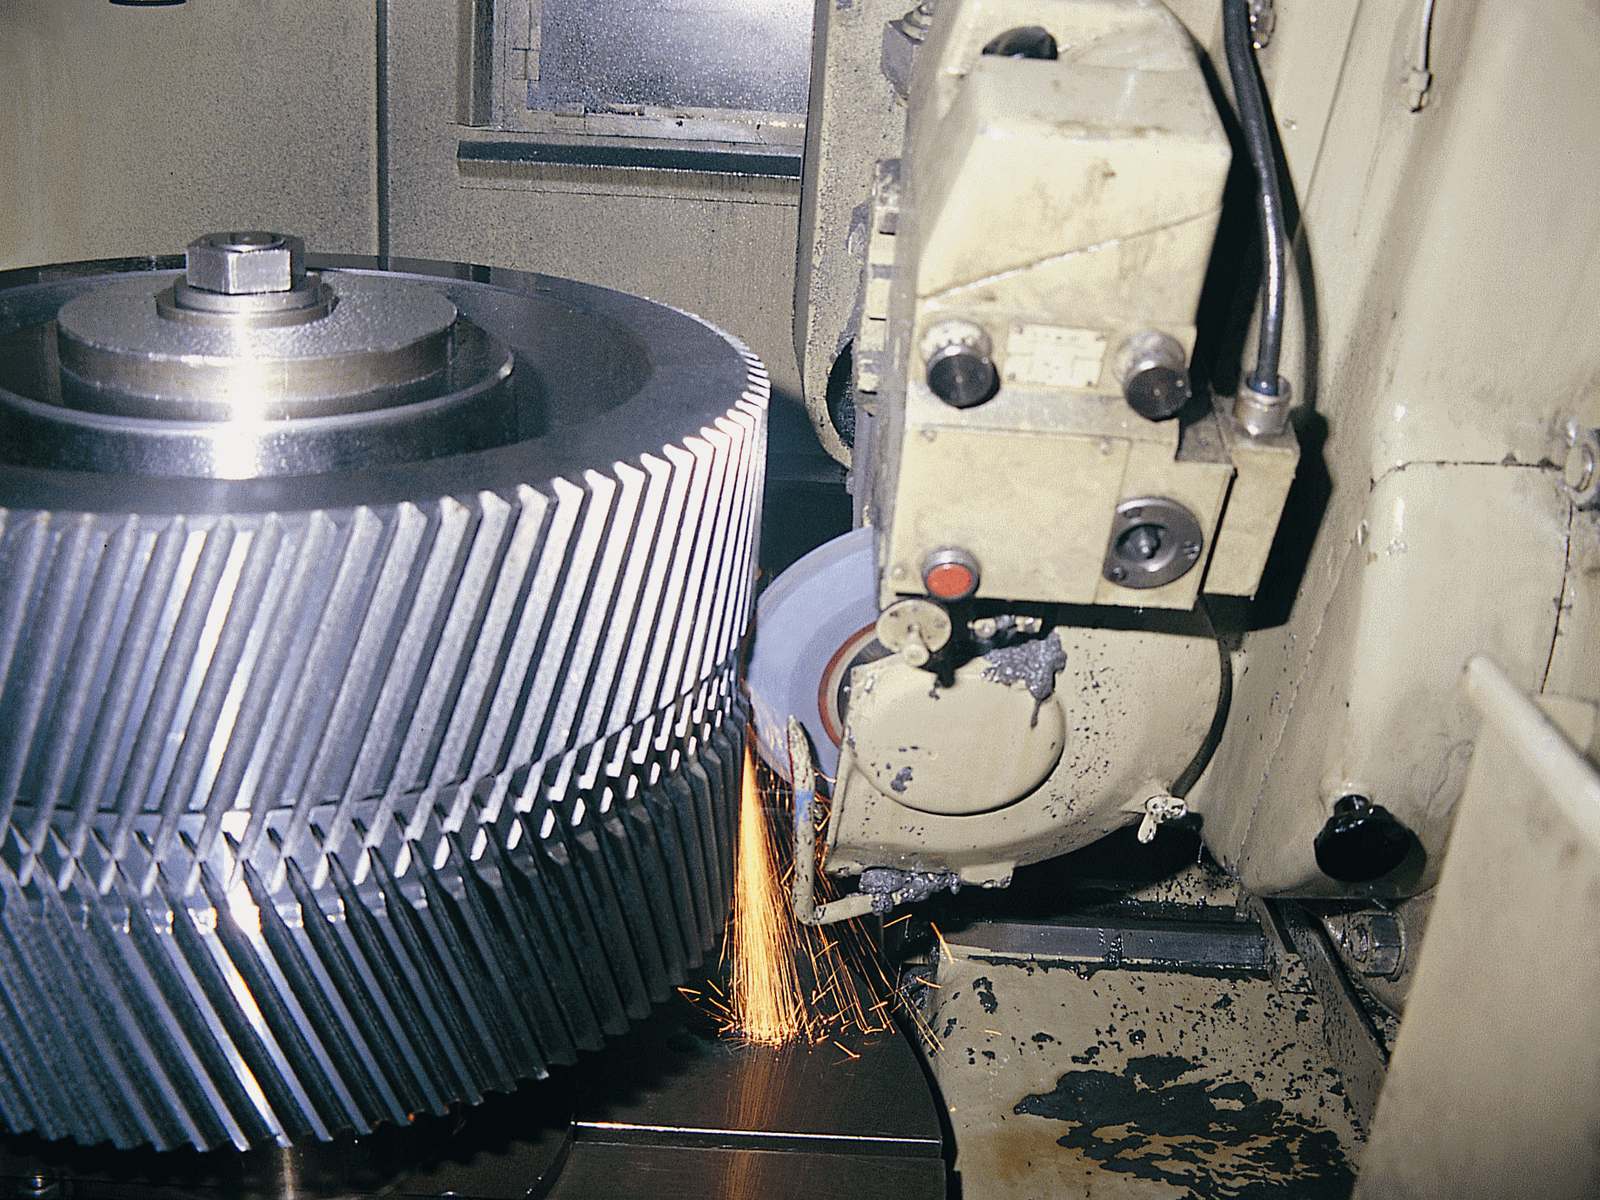
Gear cutting is the core of the company’s work since 1965. We hob spur, helical and double-helical gears, generate spiral bevel gears, cut worm wheels (including multi-start wheels with a tangential head) and produce internal ring gears and special gears. Case-hardened gears are finished by tooth-flank grinding where the drawing requires it. See industrial gears for the full range.
- Spur, helical and double-helical (herringbone) gears
- Straight and spiral bevel gears, crown wheel and pinion sets
- Worm and worm wheel sets, single- and multi-start; worm grinding
- Internal ring gears and planetary gear components
- Special gears: ratchets, sprockets, spline hubs, Hirth couplings
Heat treatment
In-house heat treatment under controlled conditions
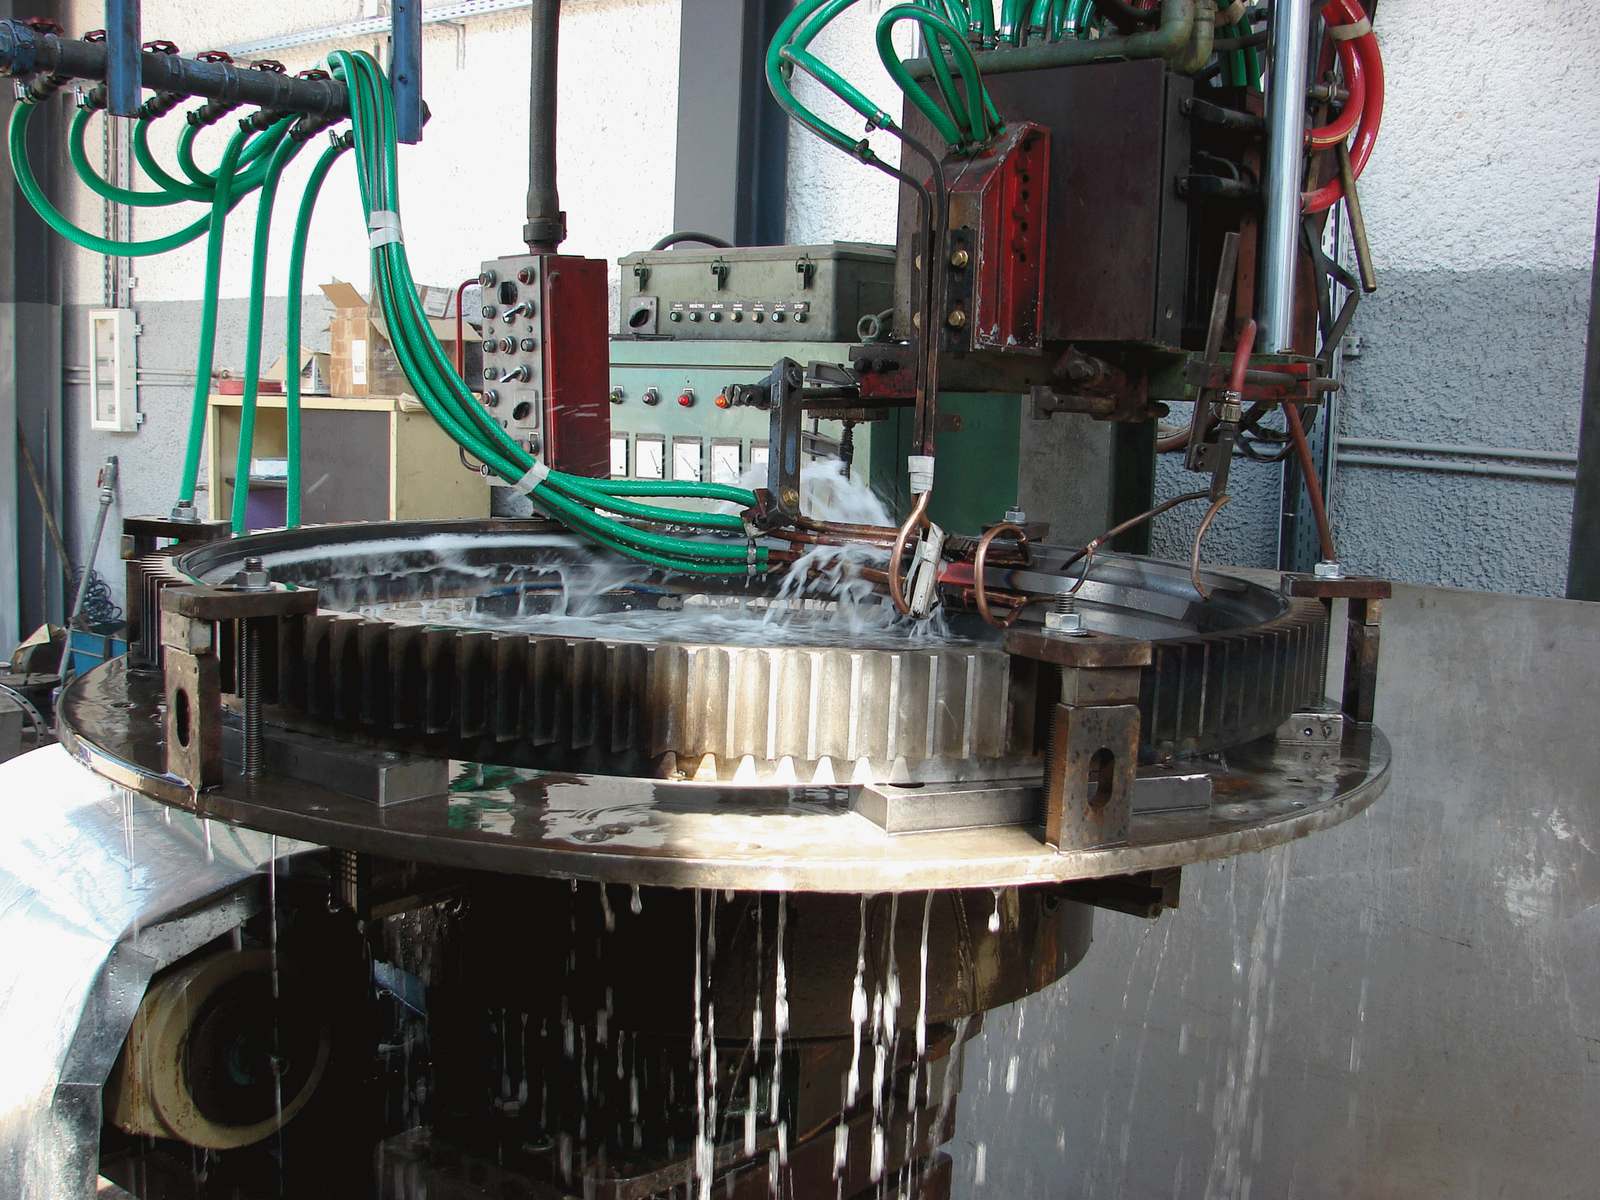
Heat treatment is carried out in our own plant, so the steel, the case depth and the grinding allowance are planned together. The gas heat-treatment centre works under protective atmosphere; carburizing cycles are designed with dedicated software and the process conditions are recorded continuously. We also heat-treat parts supplied by other companies. More on the heat treatment page.
- Gas carburizing with oil quenching and tempering
- Carbonitriding, gas nitriding (short and long cycles), gas nitrocarburizing
- Induction hardening, including tooth-by-tooth hardening of large gears
- Hardening, quenching and tempering, normalizing, ageing
- Hardening of aluminium extrusion dies
Assembly, inspection and testing
Assembled, checked and documented
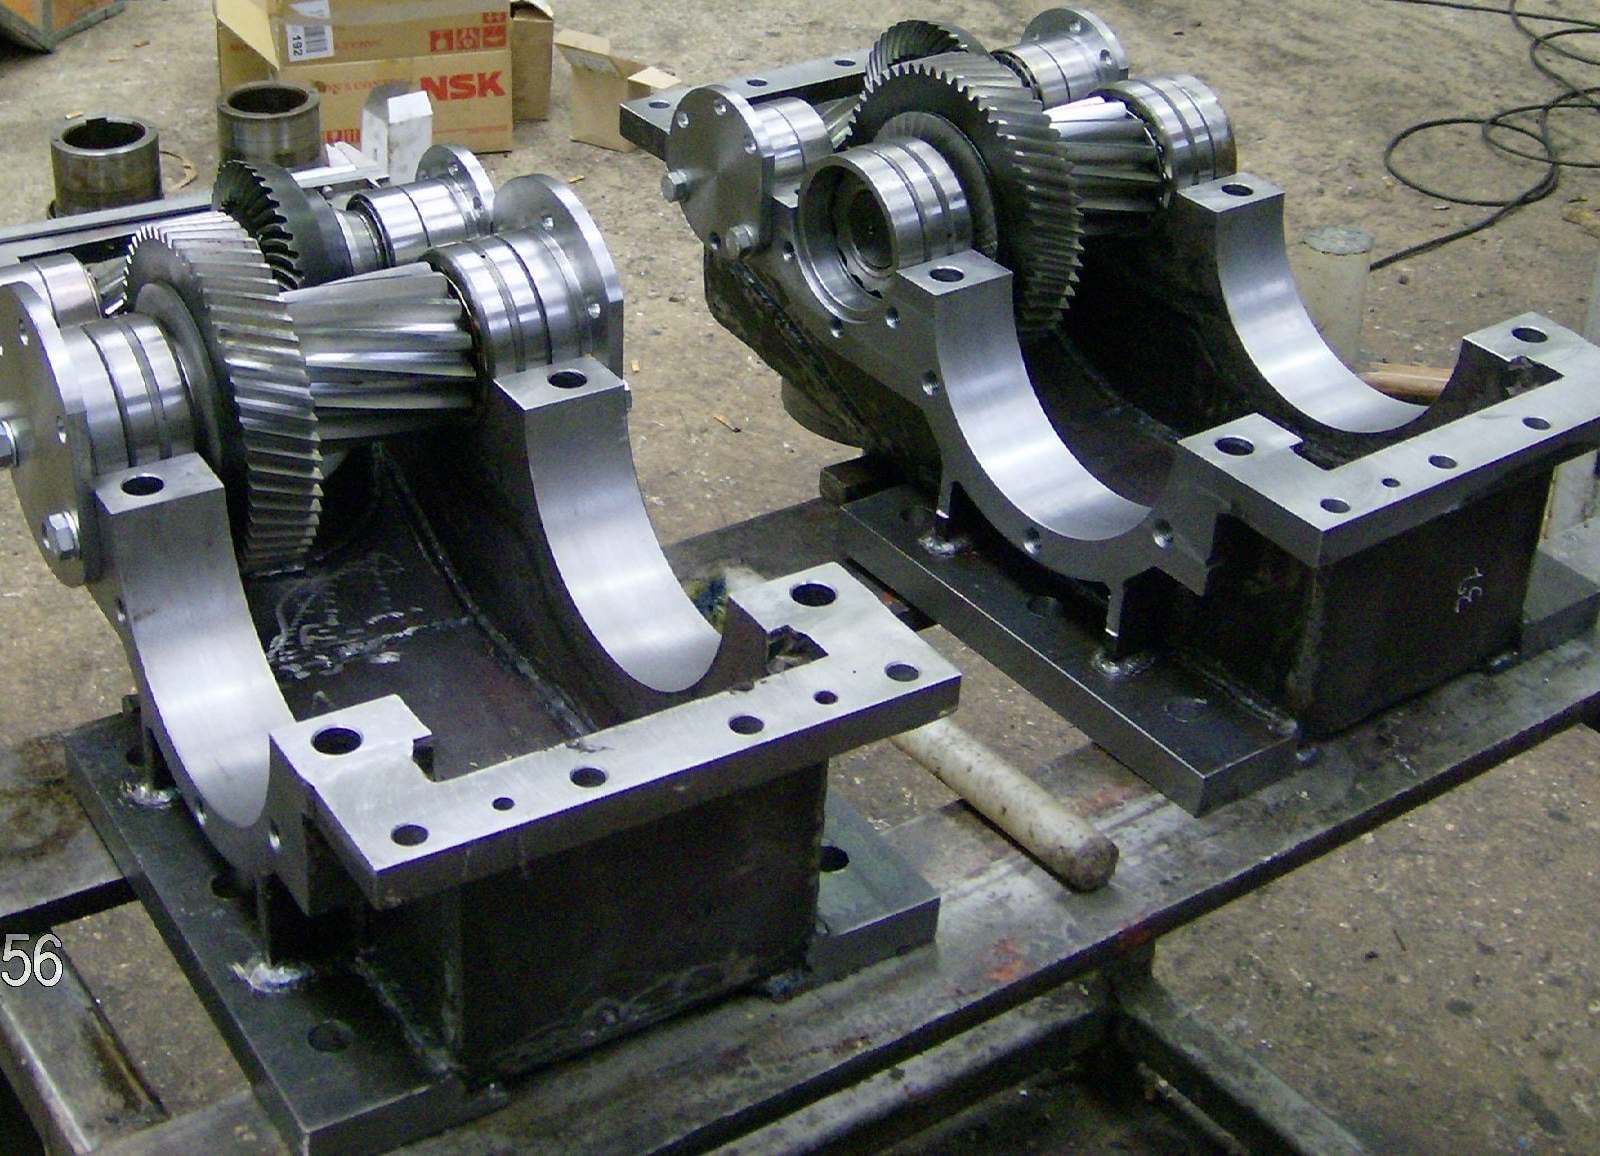
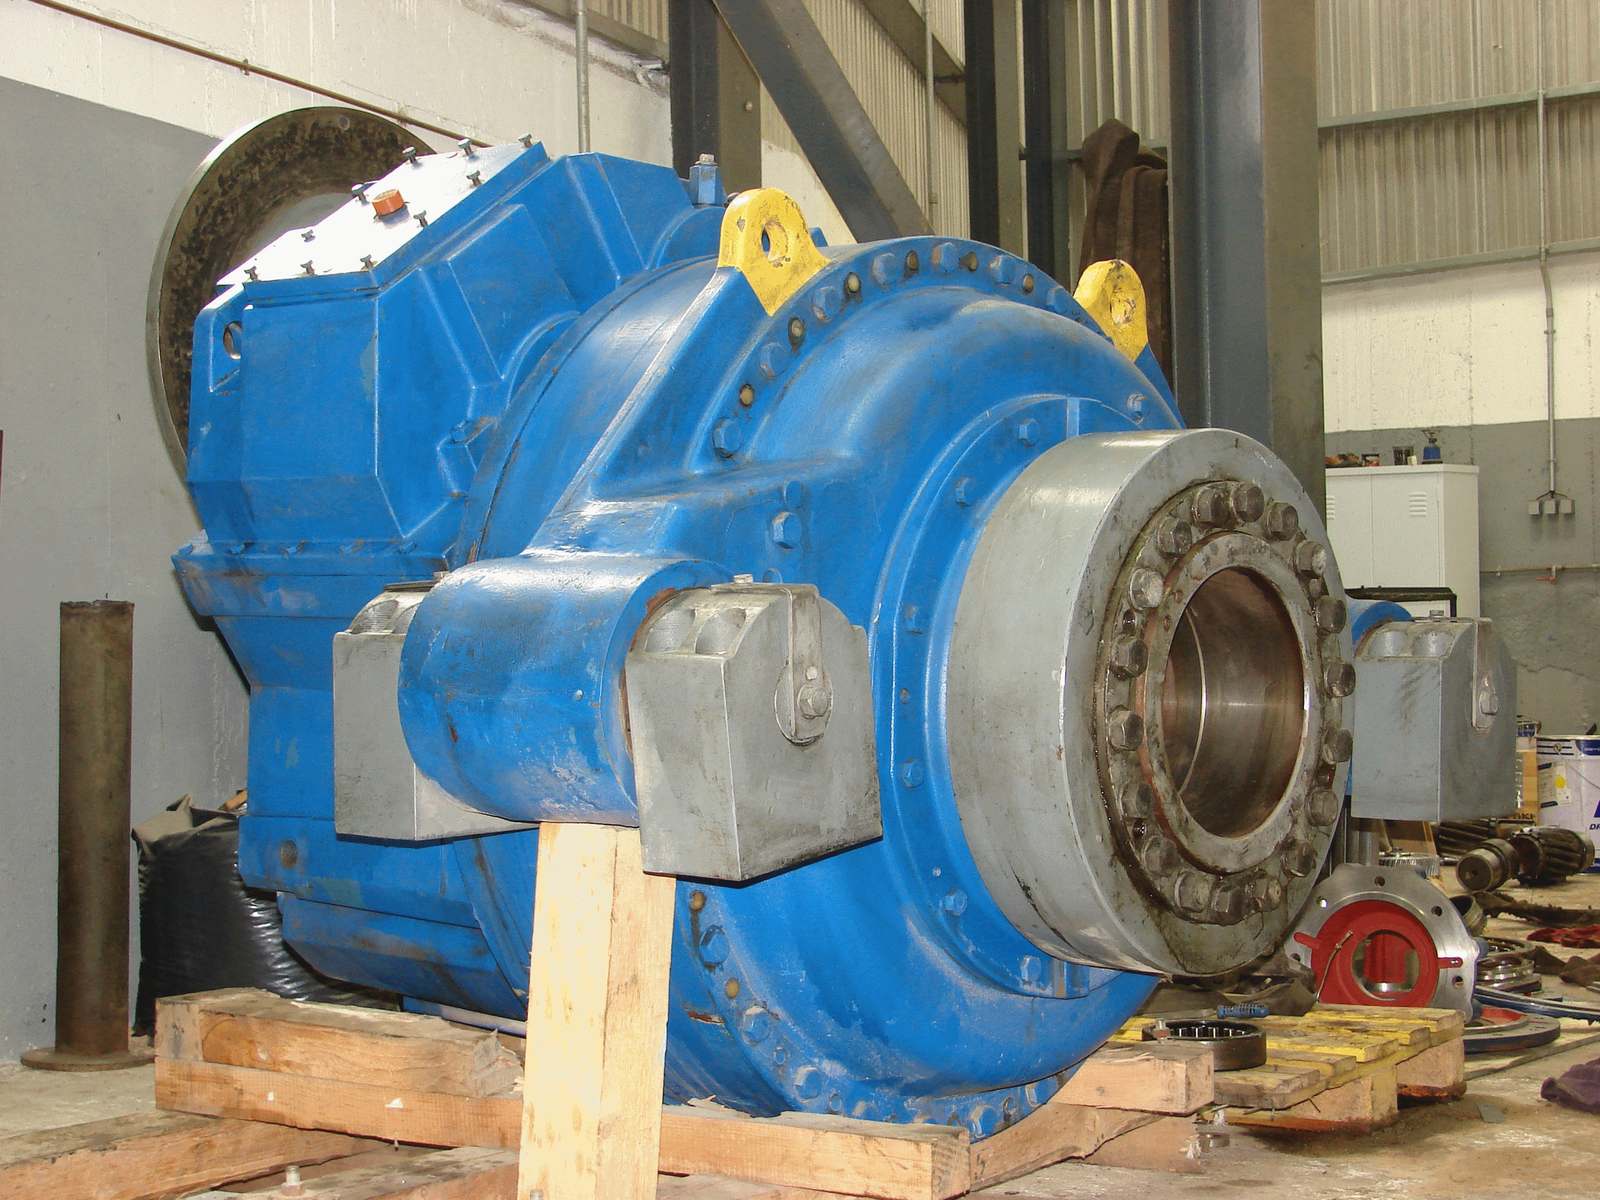
Gearboxes are assembled in our assembly department, where gear mesh and contact pattern are checked before the housing is closed. The quality control department inspects parts during production and before dispatch. Repaired gearboxes can be load-tested where required, checking lubricant and bearing temperatures and noise. Our back-to-back gearbox test rig, with test power up to 9,000 kW, monitors vibration, temperature, sound and oil cleanliness. See quality and technical approach.
- Dimensional inspection, hardness after heat treatment, surface roughness
- Surface examination for micro-cracks
- Gear tooth form inspection
- Inspection documents to EN 10204 as agreed with the order
Repair and overhaul
Repair of gearboxes and mechanical equipment
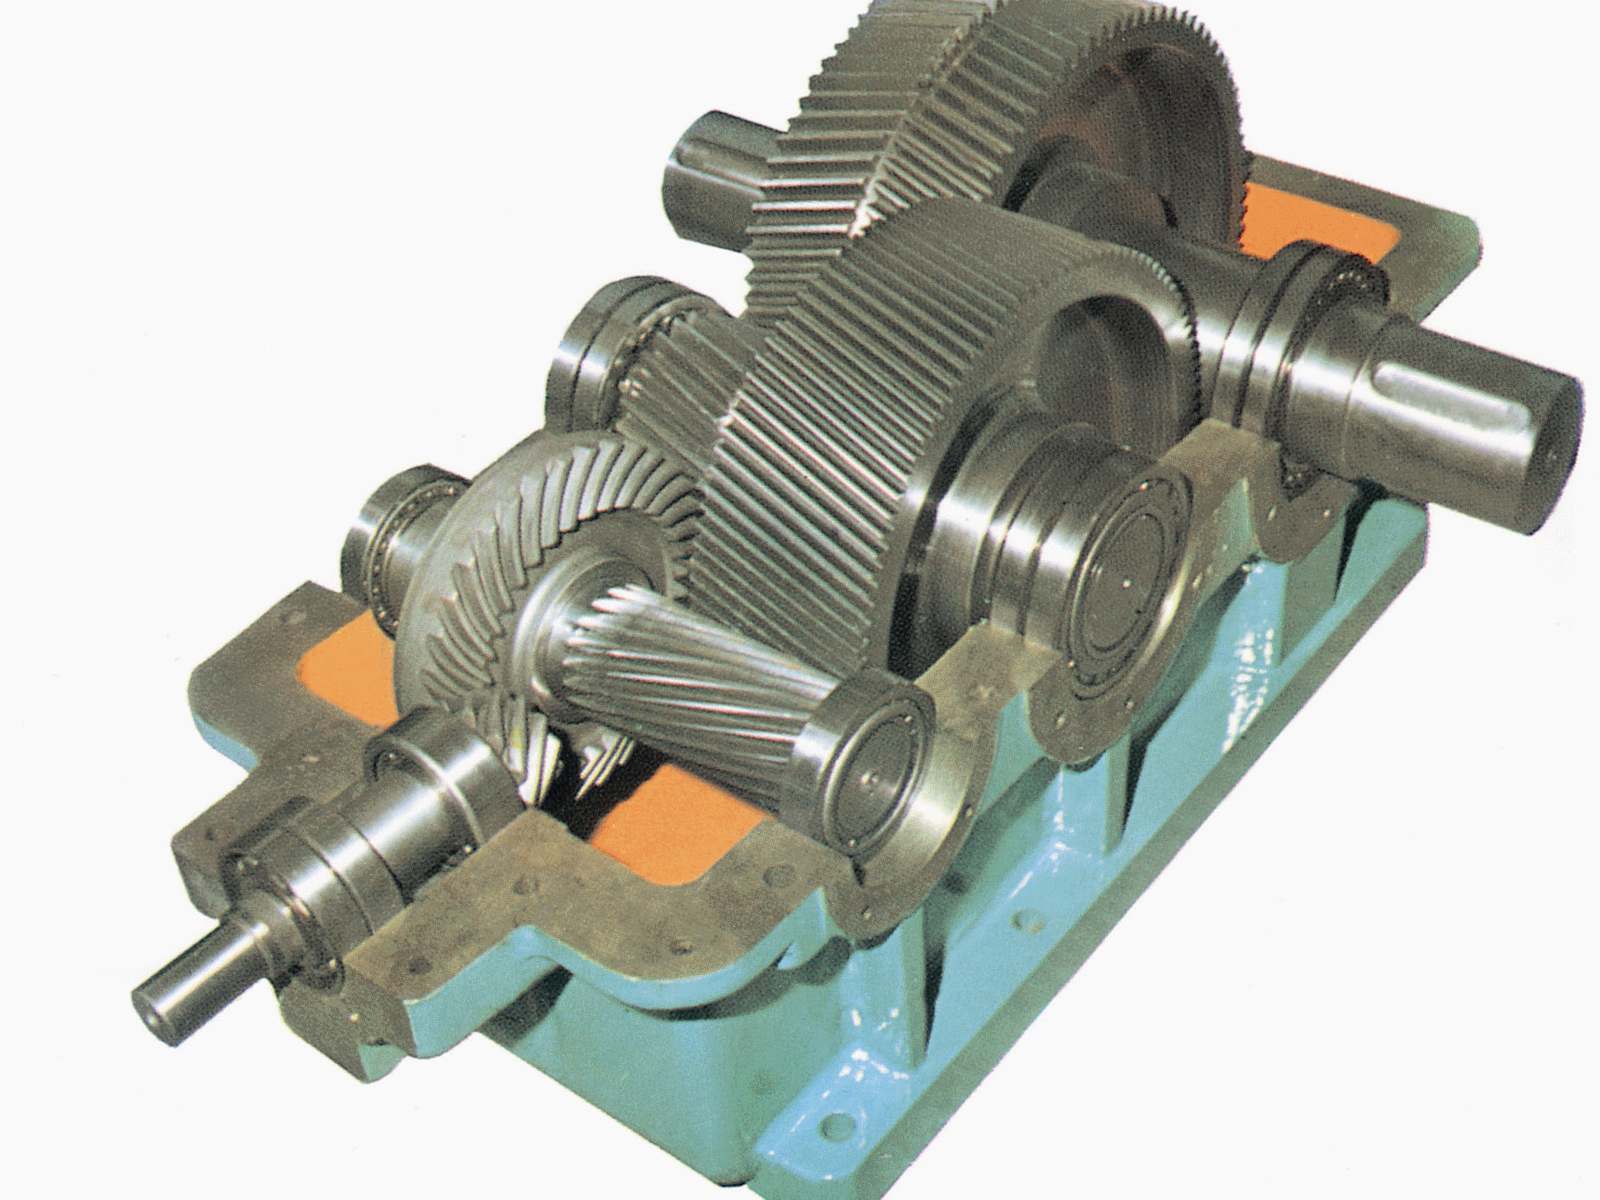
We inspect, dismantle, repair and reassemble industrial gearboxes in our workshop and manufacture the gears, shafts and bushes they need. Shafts can be rebuilt by welding or metallizing and ground back to size; damaged gears can receive a new toothed rim on the existing body. A maintenance report records the gearbox type and serial number, the work done and the parts replaced. Read more on gearbox repair and overhaul and industrial mechanical repair.
- Parallel-shaft, bevel-helical and planetary gear units
- Gear repair and replacement, shaft repair and replacement
- Housing repair by welding and re-machining
- Reconditioning of extruder screws and barrels
Manufacturing from a drawing or from a sample
We do not sell catalogue products: every part is made to your specification.
-
Drawing or sample
Send a drawing with tolerances, material and heat treatment, or a sample or worn part when no drawing exists.
-
Measurement and data
For a sample we measure the part, determine the gear data and identify what must be clarified, such as material and hardness.
-
Drawing and approval
We prepare or complete the production drawing and agree it with you before manufacture.
-
Manufacture and inspection
Machining, heat treatment, grinding and inspection in our plant, with the documents agreed in the order.
Documented capacities
Key figures for our gear cutting, machining, heat treatment and gearbox testing equipment.
| Process | Capacity |
|---|---|
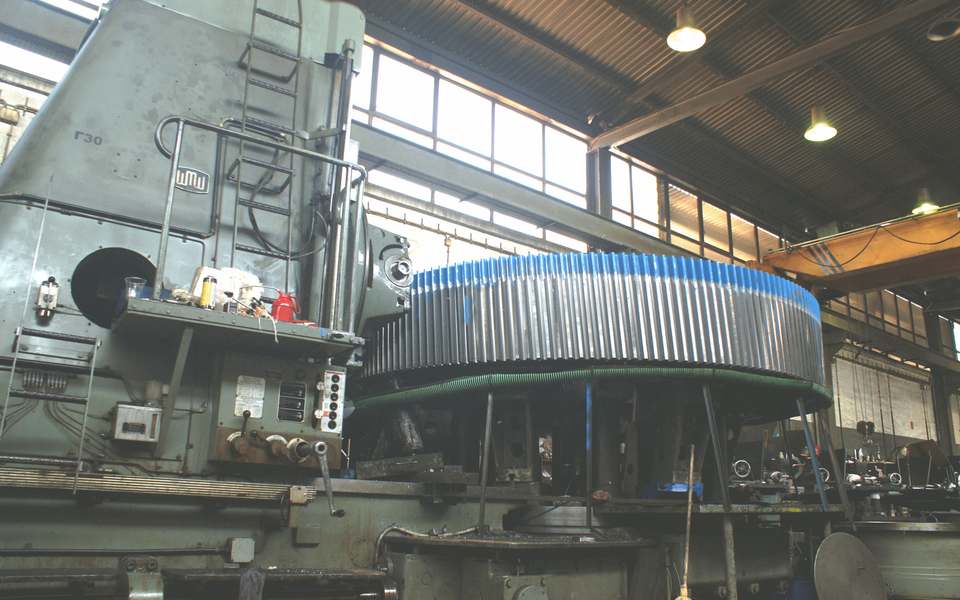
| Gear cutting (double-helical / herringbone) | Outside diameter up to 4 m, module 1 to 20 |
| Spiral bevel gear generation | Outside diameter up to 1,000 mm, module up to 13 |
| Milling and boring workpiece envelope | 3.5 × 7 × 5 m |
| CNC machining centres | Horizontal 4-axis centre with 60 tools; 2 CNC 4-axis centres; 1 CNC 3-axis vertical mill |
| Gas carburizing | Case hardening depth up to 2.5 mm; surface hardness 55–65 HRC, depending on steel grade and carburizing programme |
| Gas nitrocarburizing | Surface hardness 55–62 HRC, depending on material and process parameters |
| Gearbox test rig (back-to-back) | Test power up to 9,000 kW |
In the workshop
-
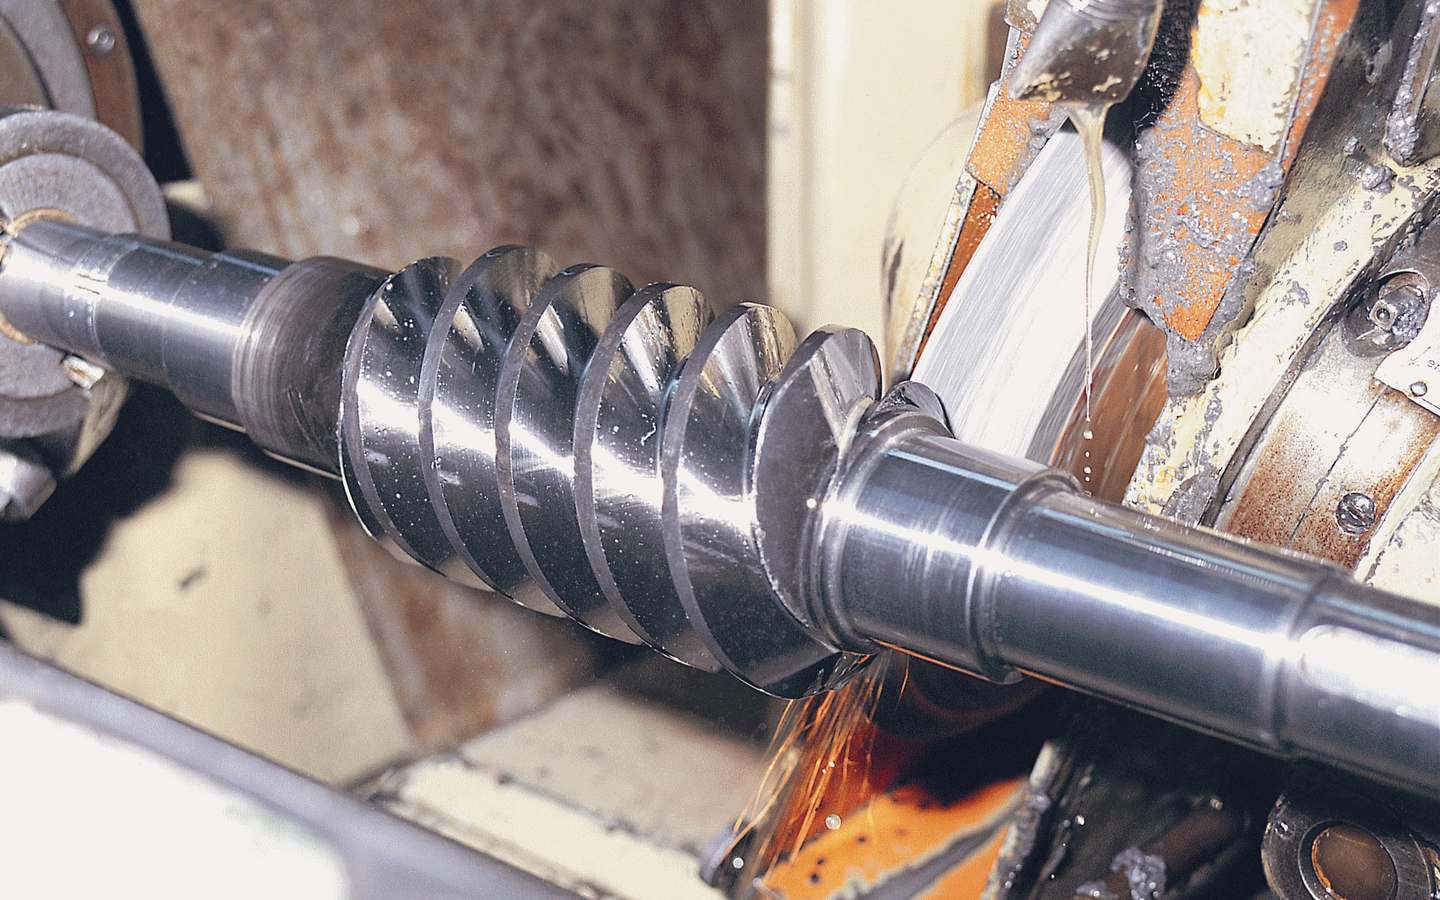
Worm shaft being ground on a thread grinding machine with coolant and sparks -
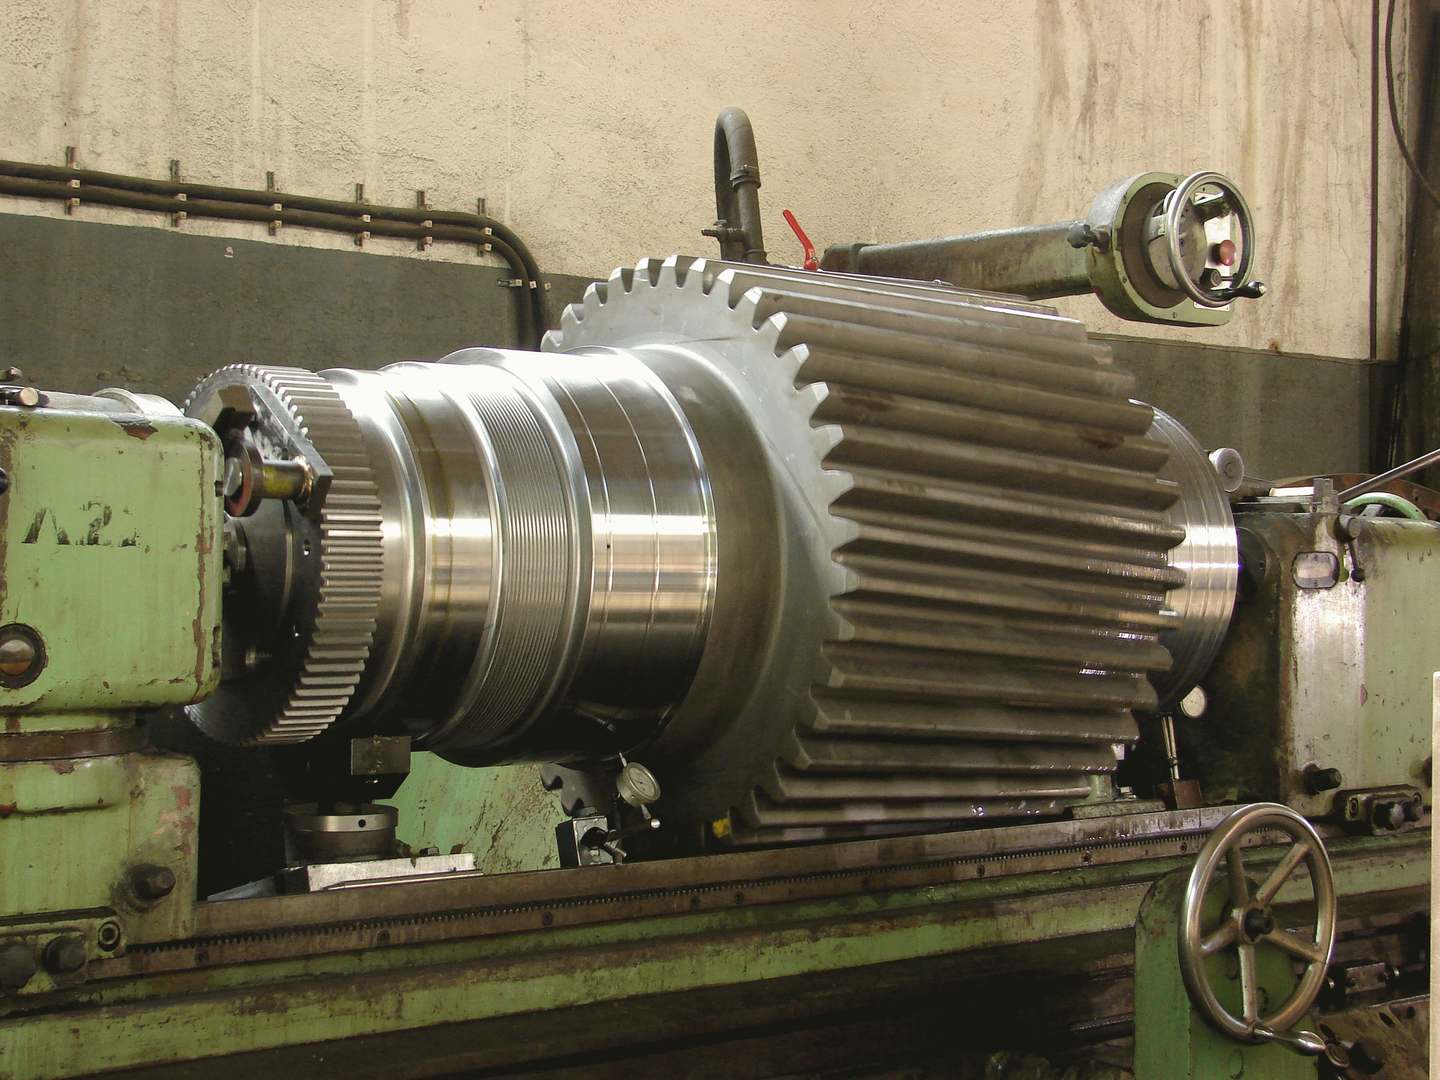
Large spur pinion shaft mounted on a cylindrical grinding machine for journal grinding -
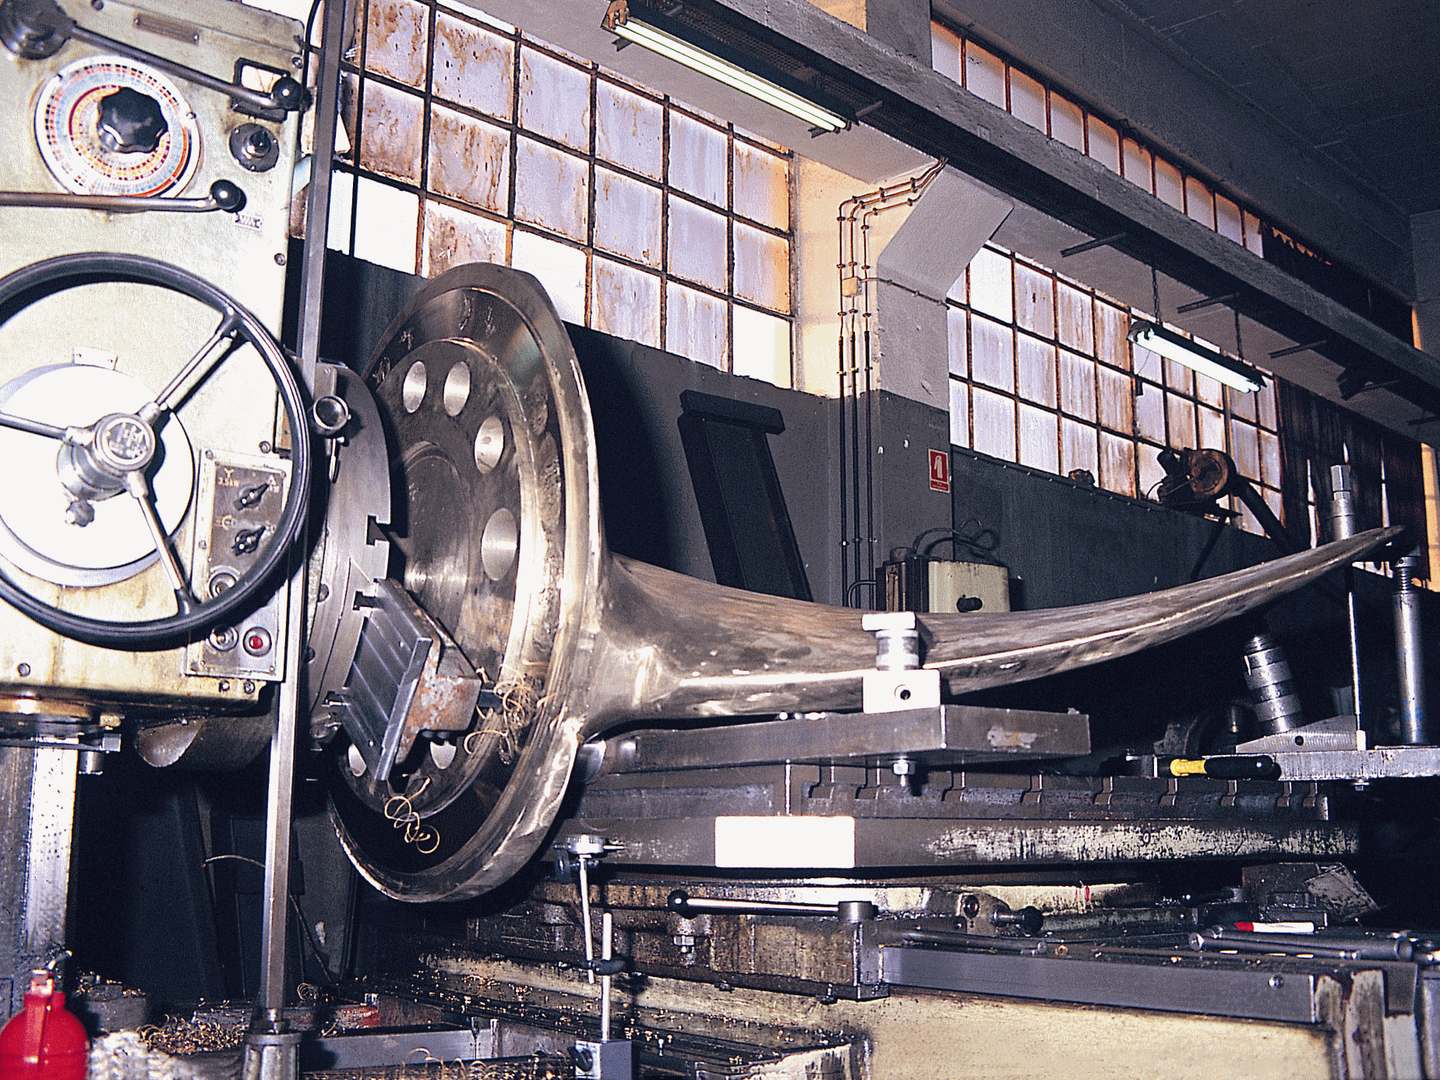
Marine propeller blade flange machined on a horizontal boring mill -
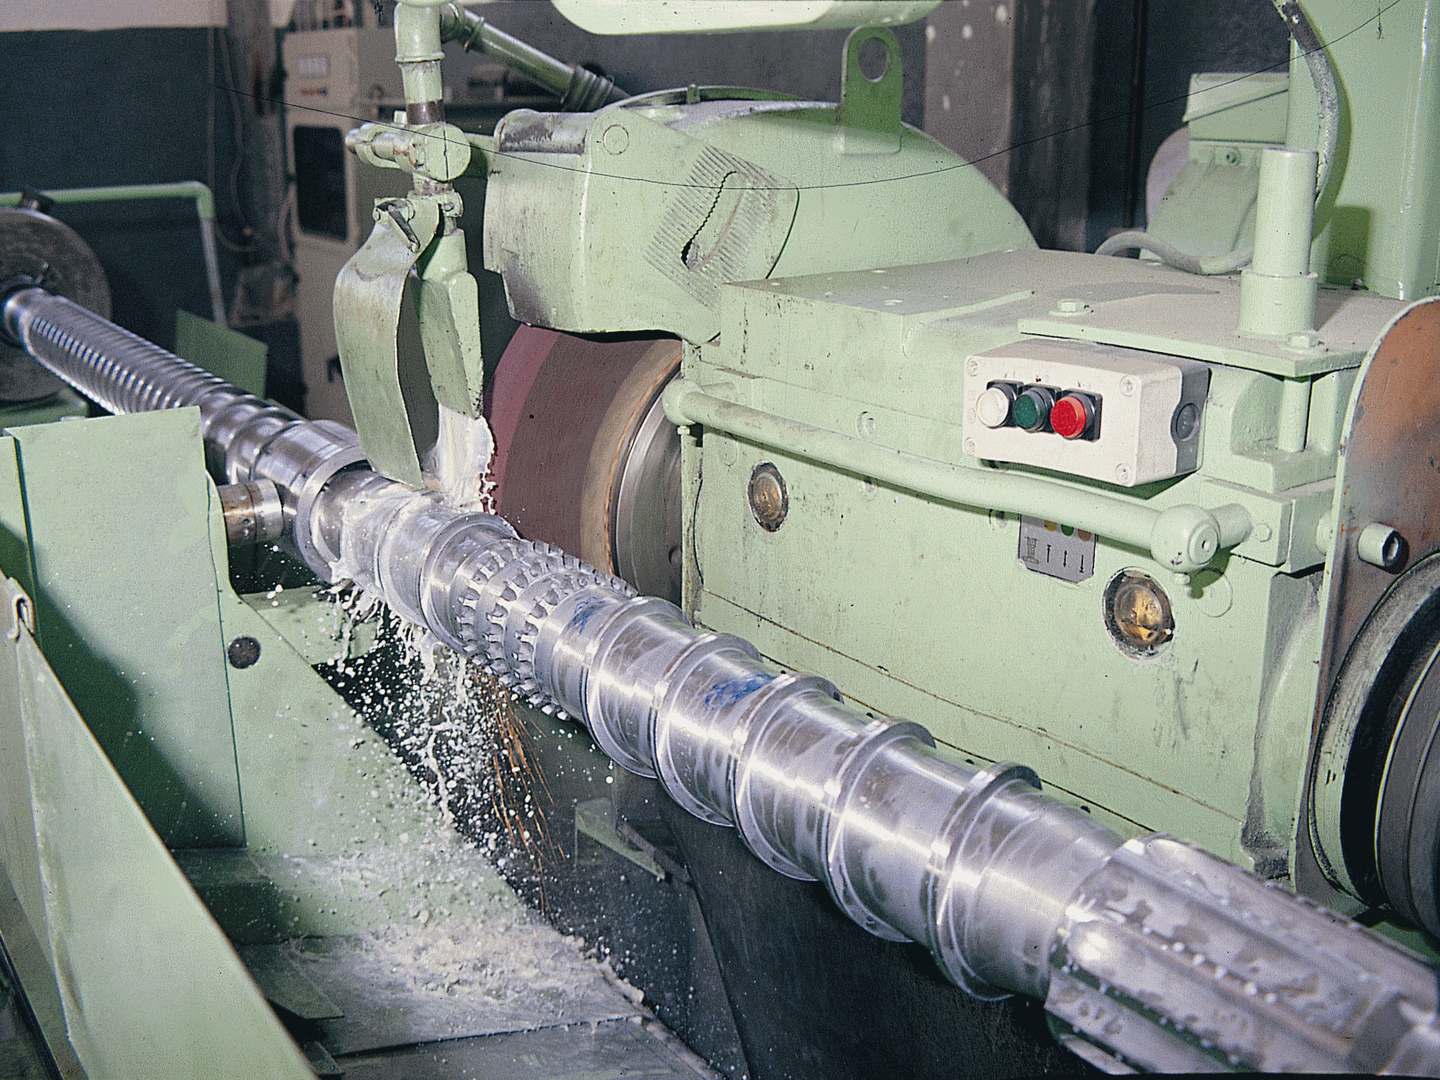
Extruder screw being ground on a cylindrical grinding machine with coolant spray
Products and services in detail
Every capability above is described in more depth on the following pages.
-
Industrial Gears Made to Drawing or Sample
Spur, helical, double-helical, bevel, worm and internal gears, pinion shafts and special gears, made to drawing or sample with in-house gear cutting, heat treatment and grinding. -
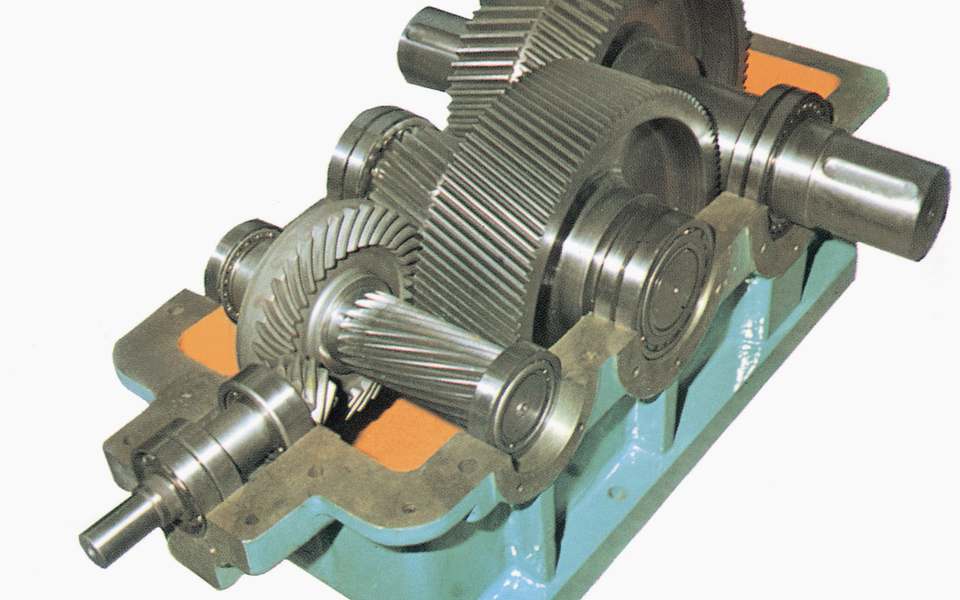
Gearboxes & Speed Reducers
Custom parallel-shaft and bevel-helical gearboxes, planetary gear components, gearbox parts, and repair, refurbishment and upgrading of existing industrial gear units. -
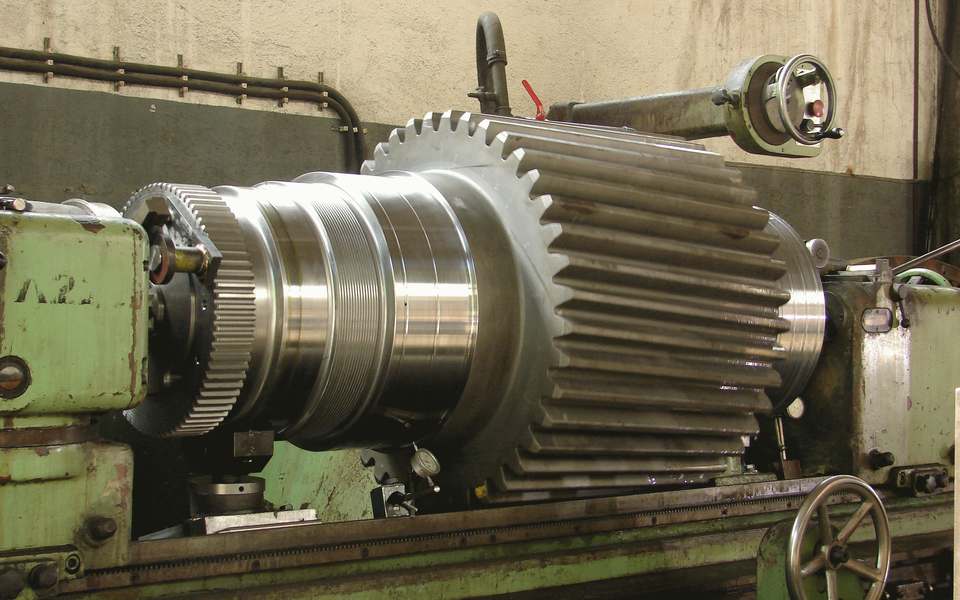
Shafts, Pinion Shafts and Splined Shafts
Shafts, pinion shafts, splined shafts and long shafts made to drawing or sample, with in-house gear cutting, heat treatment and grinding. -
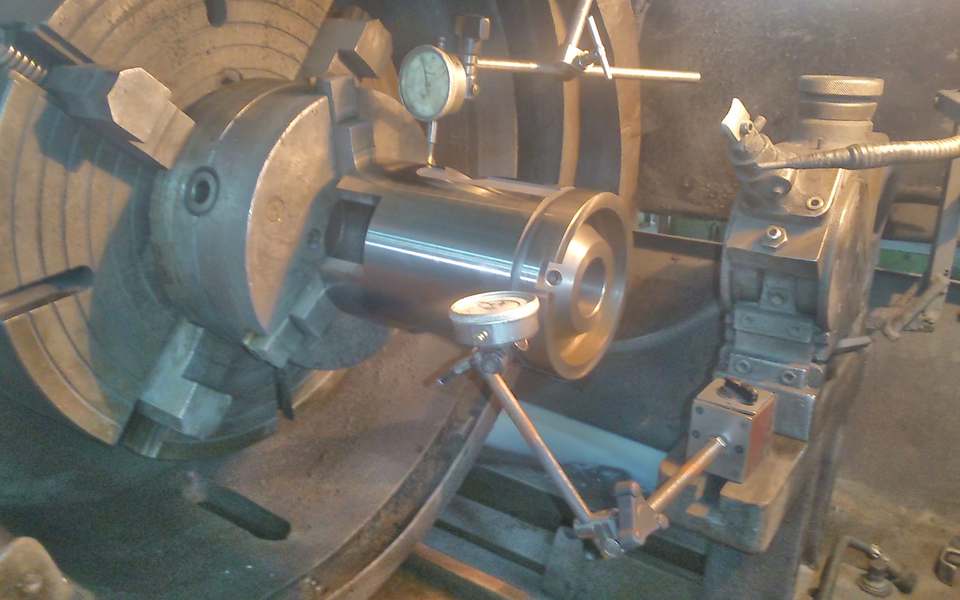
Industrial Transmission Components
Couplings, splined hubs, pulleys, sprockets, bushes, rings, worm wheels and Hirth couplings made to drawing or sample to fit your existing drive. -
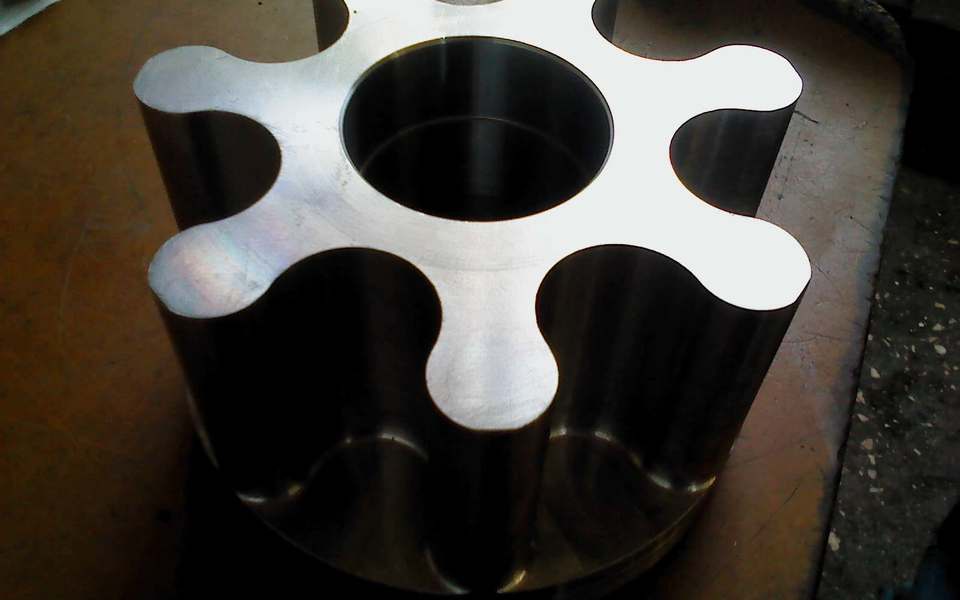
Custom Machined Components to Drawing
Special components machined to drawing — rotors, rings, flanges, drums, housings, dies, propeller parts — with in-house heat treatment and grinding. -
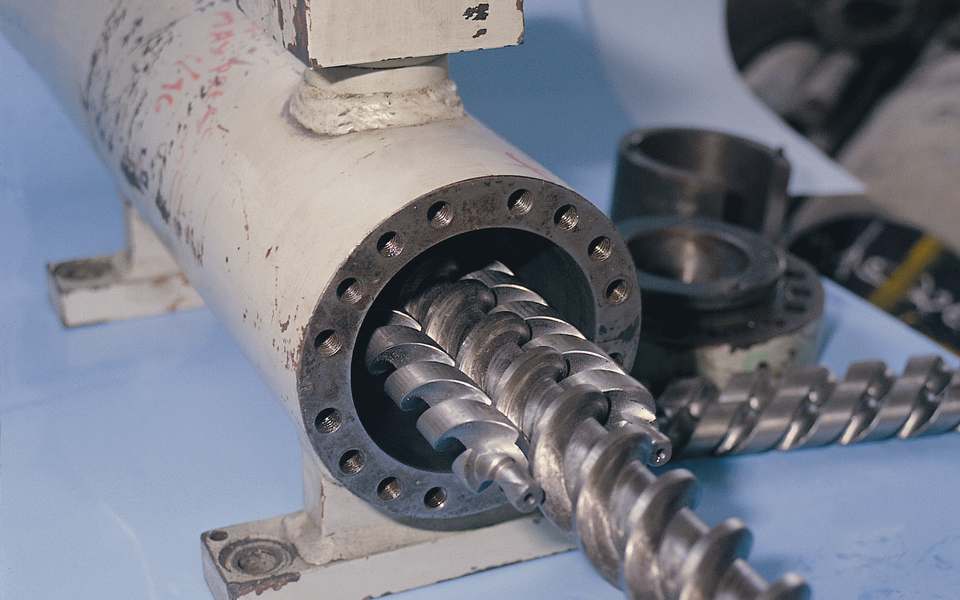
Extruder Screws and Barrels
Extruder and injection screws, single and twin barrels, valve heads and dies, made to drawing or sample, nitrided in-house and reconditioned when worn. -
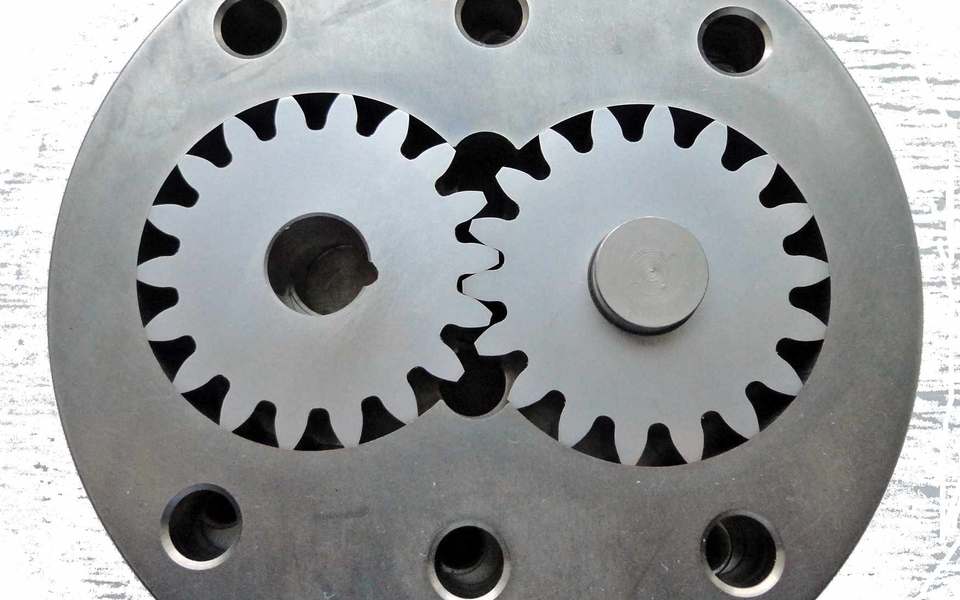
Industrial Spare Parts Made to Drawing or Sample
Replacement gears, shafts, bushes, pump parts and obsolete OEM components made from drawing or worn sample, for plants in Greece and abroad. -
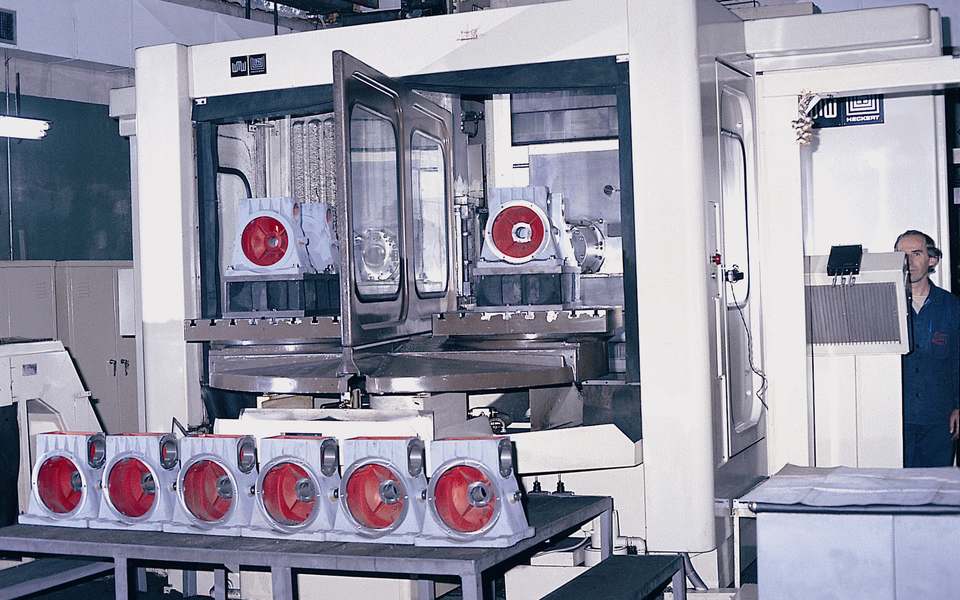
Precision CNC Machining and Conventional Machining
CNC milling on machining centres plus conventional turning, boring, thread cutting and grinding of shafts, housings, rings and gear blanks, made to drawing in Greece. -
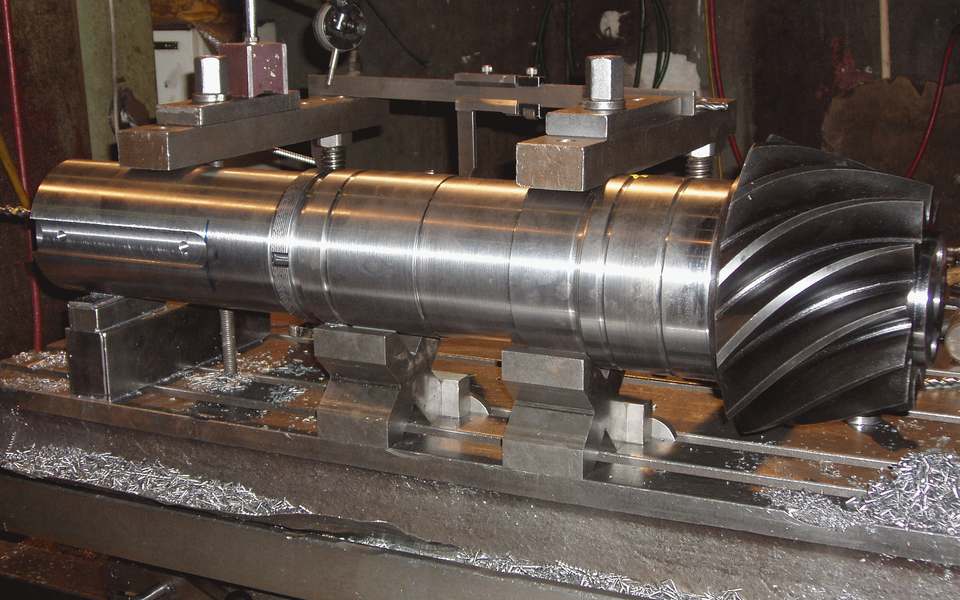
Manufacturing to Customer Drawings: Gears, Shafts and Machined Parts
Build-to-print manufacturing of gears, shafts and machined parts: drawing review, clarification of tolerances, material, heat treatment, machining and inspection. -
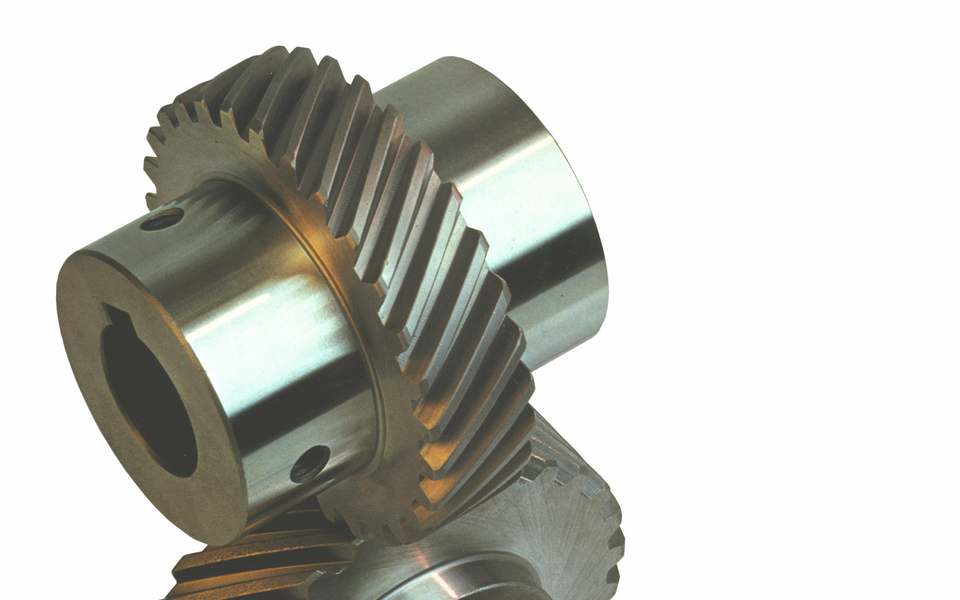
Reverse Engineering: Manufacturing Spare Parts from a Sample
Replacement parts made from a sample or worn part: measurement, gear data determination, material identification, drawing for your approval and manufacture. -
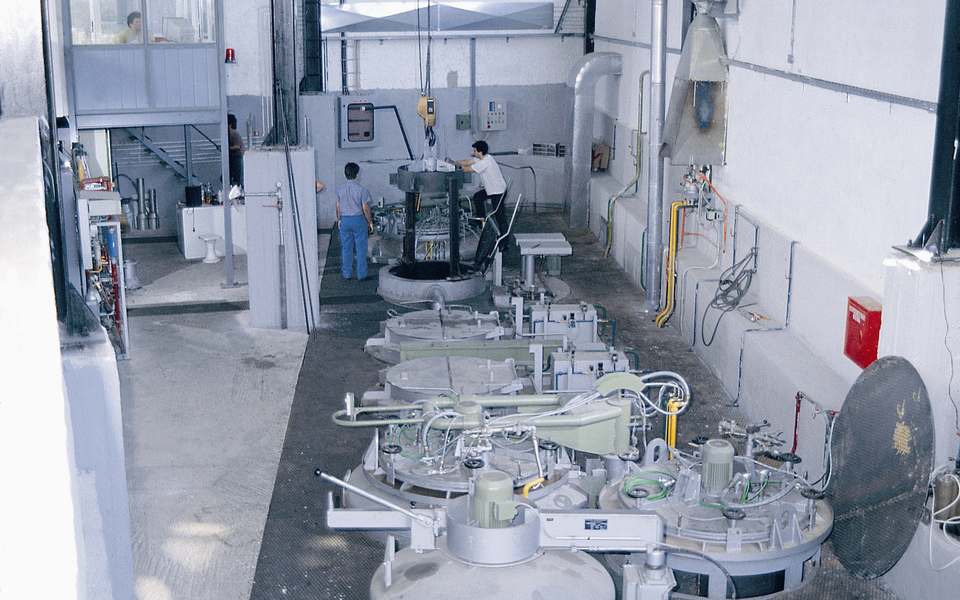
Heat Treatment: Gas Carburizing, Nitriding and Induction Hardening
Gas carburizing, carbonitriding, nitriding, nitrocarburizing, induction hardening and quenching and tempering, for our own parts and for parts supplied by customers. -
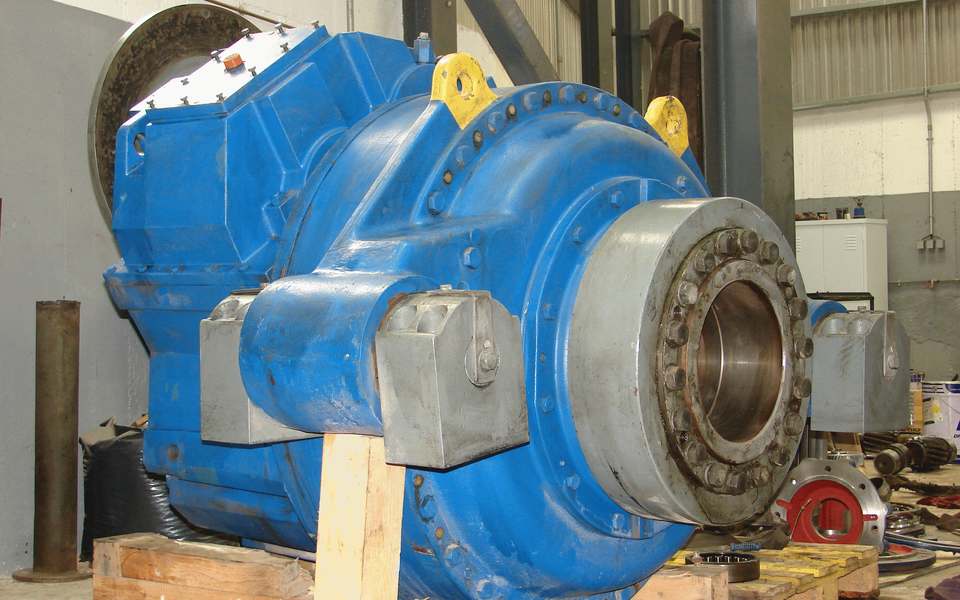
Industrial Gearbox Repair and Overhaul
Inspection, dismantling, damage analysis and overhaul of industrial gearboxes, with new gears and shafts made in-house and a maintenance report for each unit. -
Industrial Mechanical Repair: Pumps, Gears, Shafts and Extruder Parts
Repair and reconditioning of pump components, gears, shafts, extruder screws and barrels and special machine parts, or manufacture of new parts where repair does not pay.
Check whether we can make your part
Send a drawing, a sample description or photos with the main dimensions. We reply with questions or a quotation.
Please attach your technical drawings and specifications to your email.